Elevated-Temperature Strength
304H and 347H provide controlled carbon levels for improved creep and stress-rupture performance at elevated temperatures.
Nickel Alloy
TA2 / ASTM Grade 2 / TC4 / ASTM Grade 5 / TB3
Precipitation-Hardening Stainless Steel
17-4PH / Type 630 / UNS S17400
Duplex & Super Duplex Stainless Steel
Super Austenitic Stainless Steel
904L / 254 SMO / Alloy 926
High-Temperature & Stabilized Austenitic Stainless Steel
304H / 304N / 316Ti / 321 / 347 / 347H
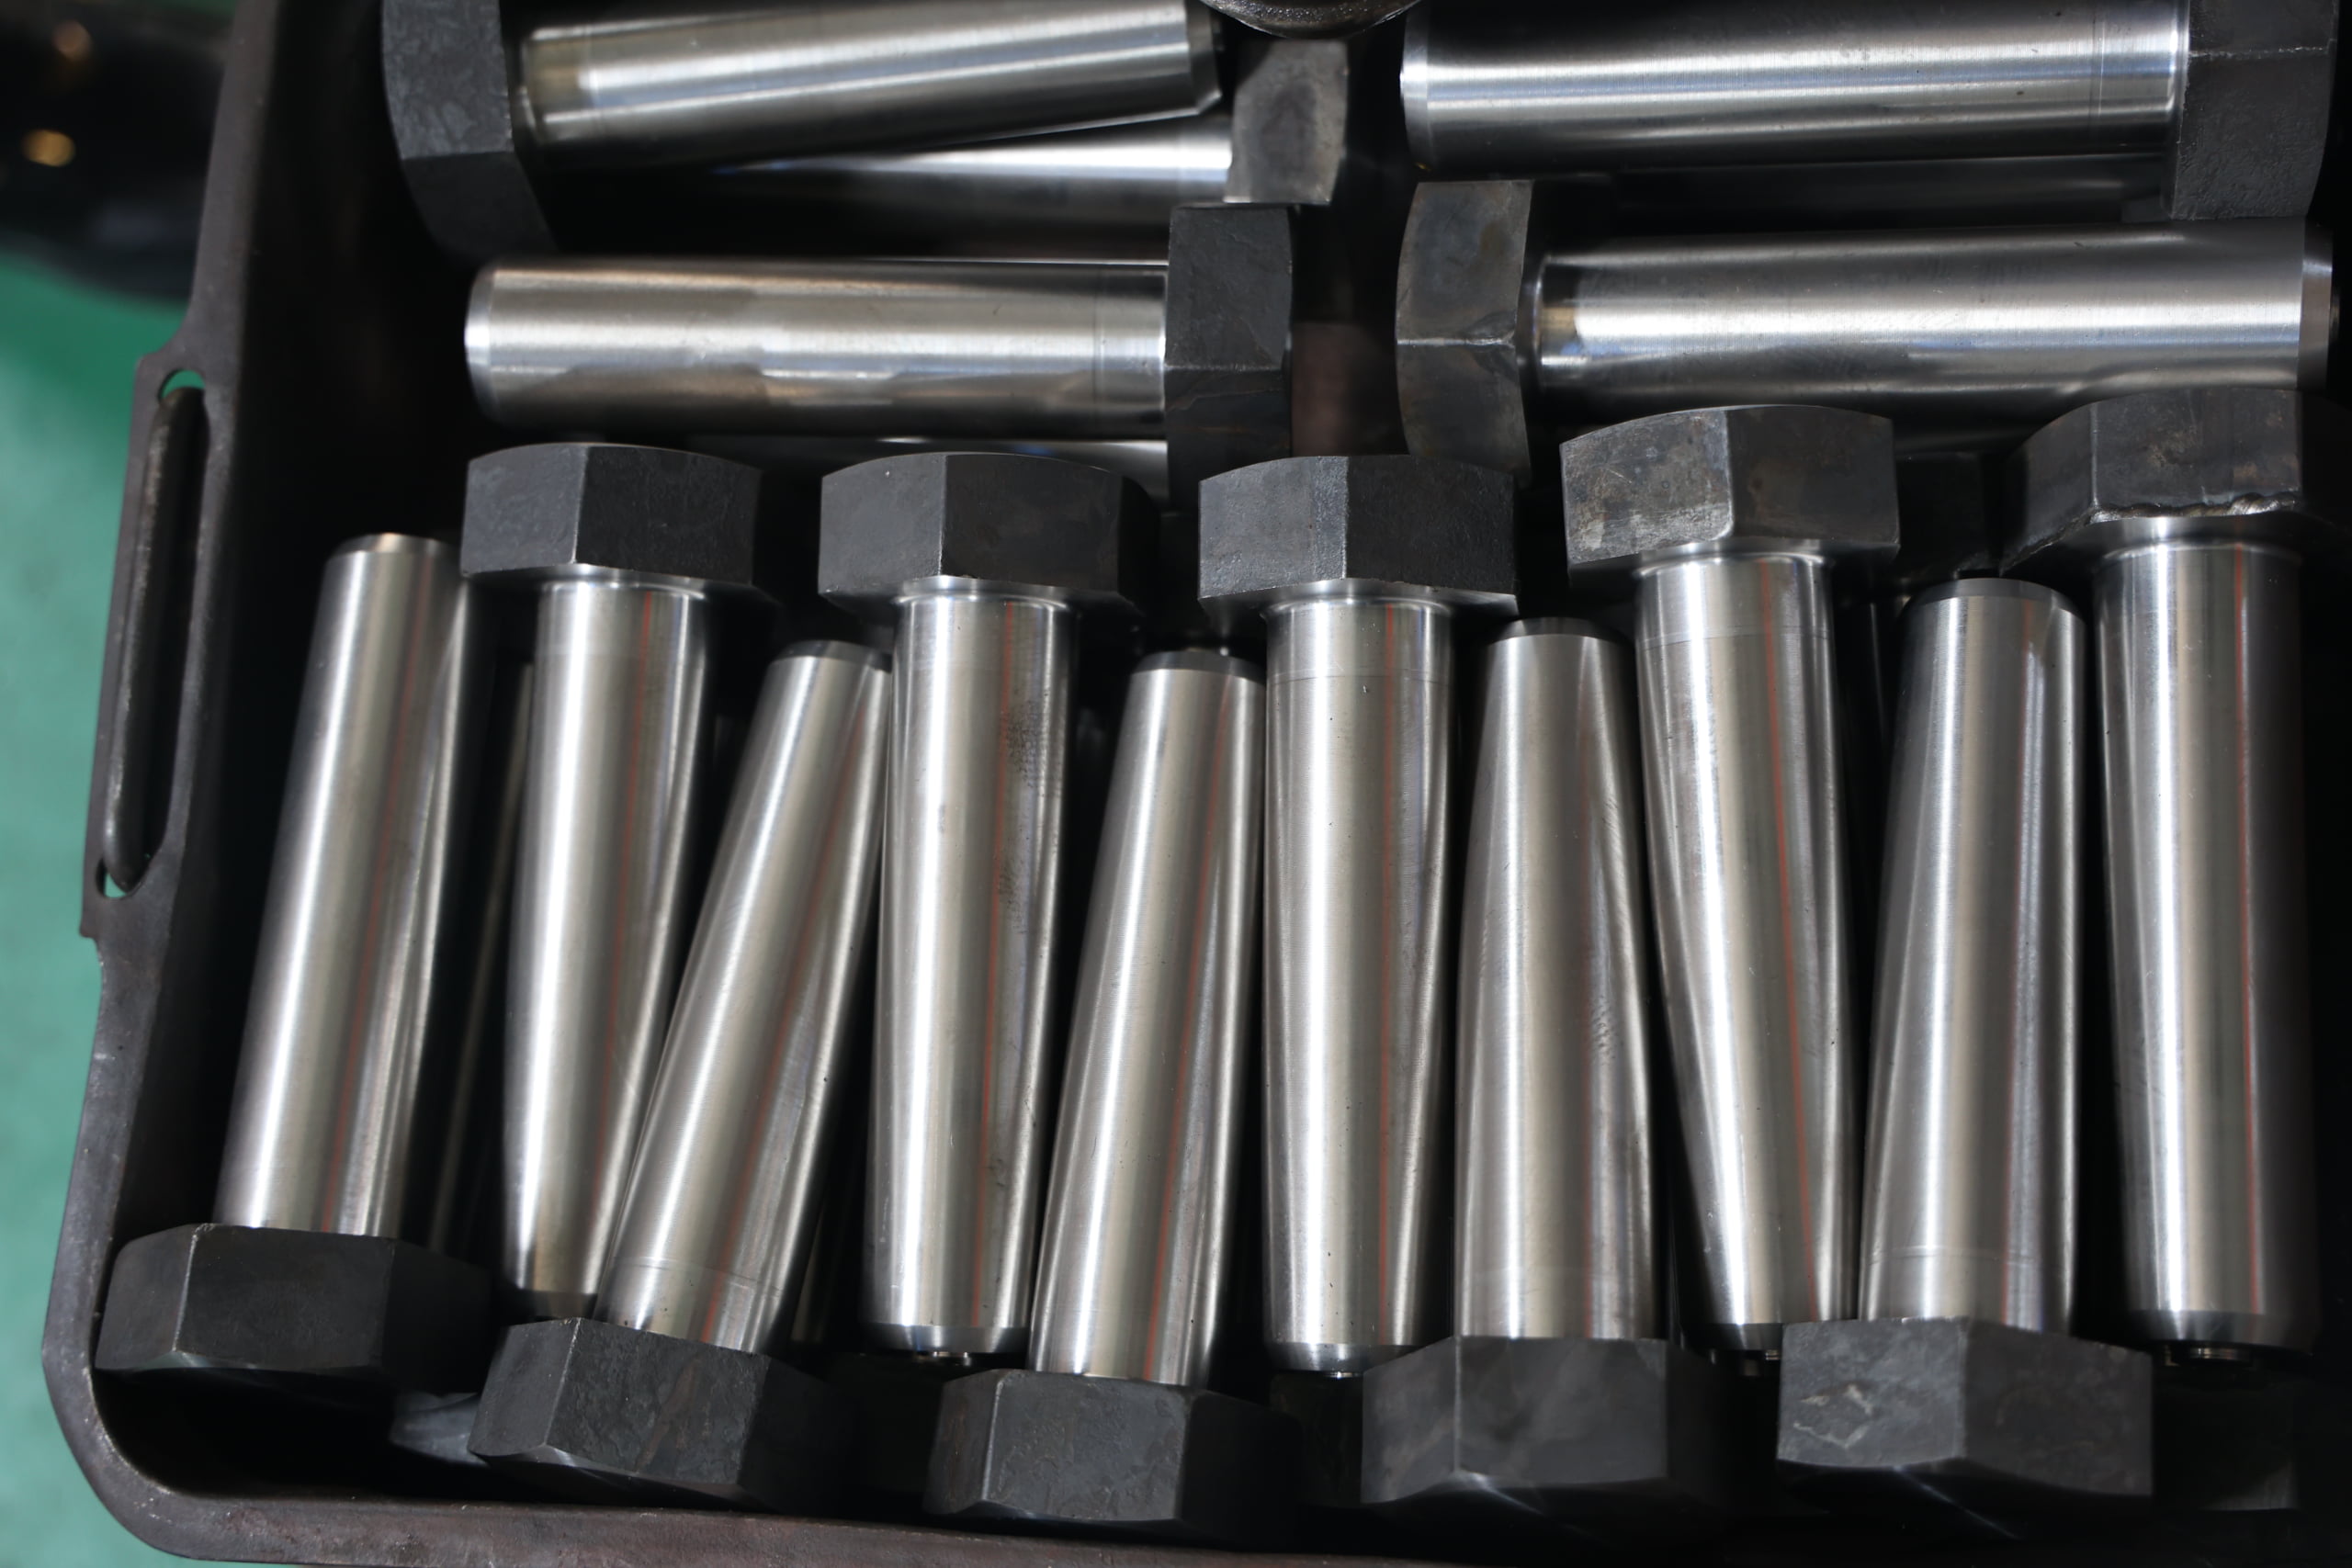
High-performance stainless steel bolts, stud bolts and custom fasteners engineered for elevated-temperature, stabilized and high-strength industrial applications.
304H, 304N, 316Ti, 321, 347 and 347H fasteners for demanding service conditions.
Controlled carbon, nitrogen, titanium or niobium provides grade-specific strength and stability.
Standard and drawing-based stainless steel fasteners manufactured to project-specific dimensions and requirements.
This material group combines several specialized austenitic stainless steel grades developed for different elevated-temperature, corrosion and strength requirements. 304H and 347H contain controlled higher carbon levels to improve creep and stress-rupture strength at elevated temperatures. 304N uses nitrogen alloying to provide higher strength than conventional 304 and is not a stabilized grade. 321 and 316Ti use titanium stabilization, while 347 and 347H use niobium stabilization. These additions reduce susceptibility to intergranular corrosion after welding or prolonged exposure within sensitizing temperature ranges. Because these grades use different strengthening and stabilization mechanisms, the exact material designation, condition and governing specification must be confirmed for each project.
These grades provide elevated-temperature strength, intergranular-corrosion resistance and specialized mechanical performance for demanding industrial fastening systems.
304H and 347H provide controlled carbon levels for improved creep and stress-rupture performance at elevated temperatures.
Titanium- or niobium-stabilized grades reduce susceptibility to intergranular corrosion after welding and elevated-temperature exposure.
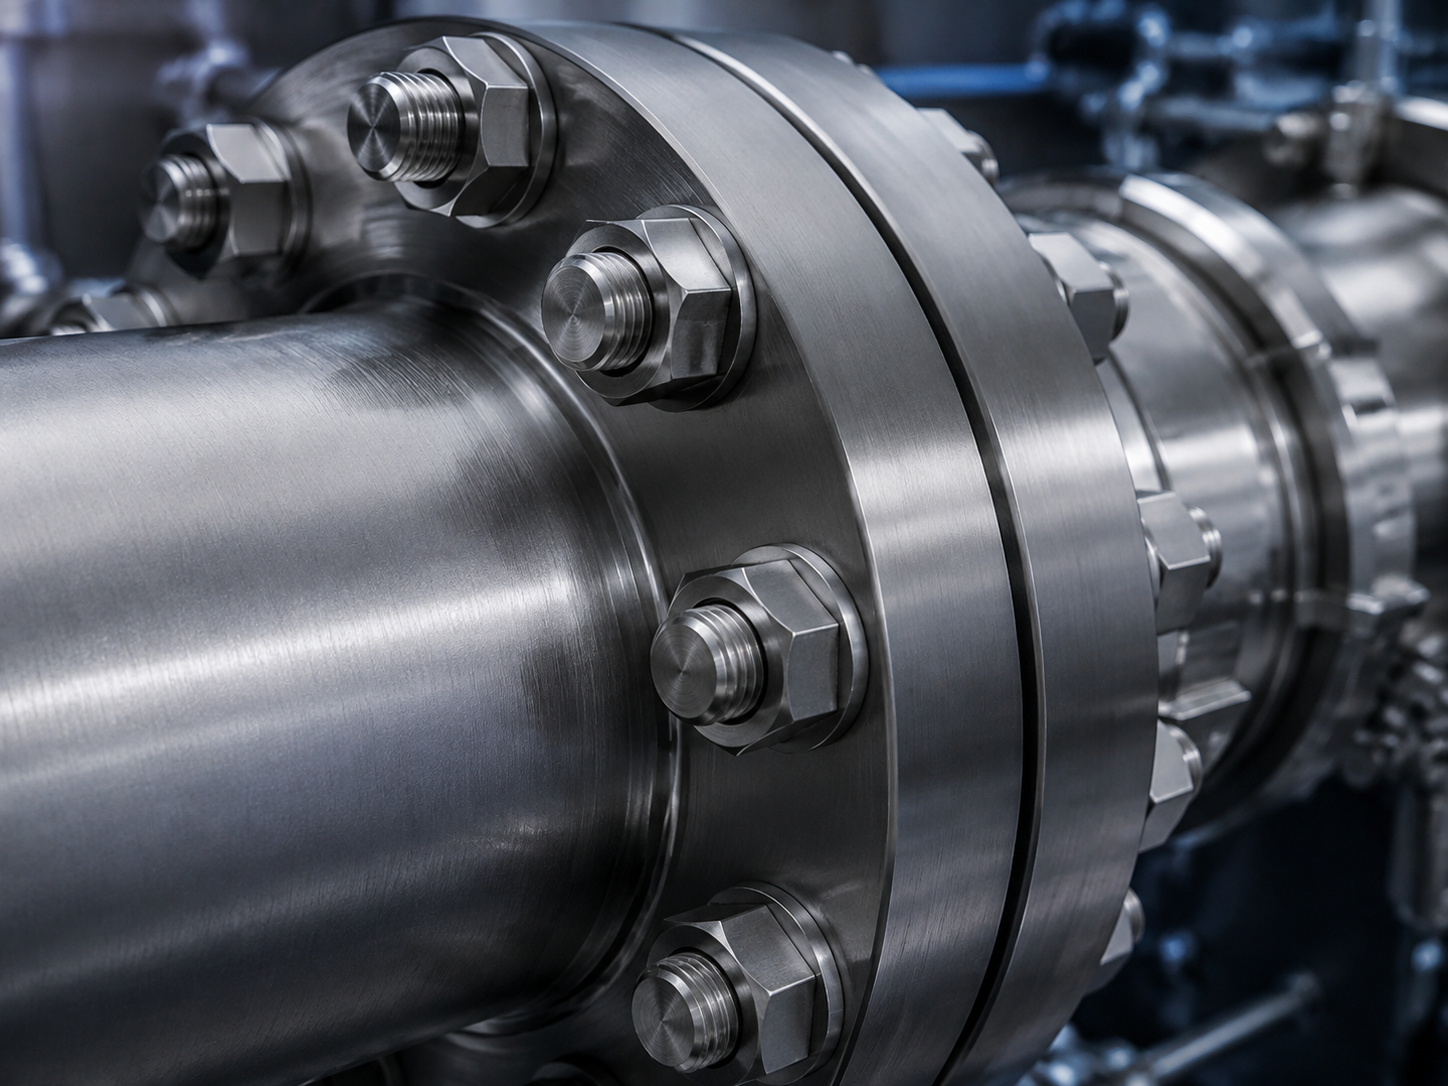
304N uses nitrogen alloying to increase yield strength while retaining useful corrosion resistance and ductility.
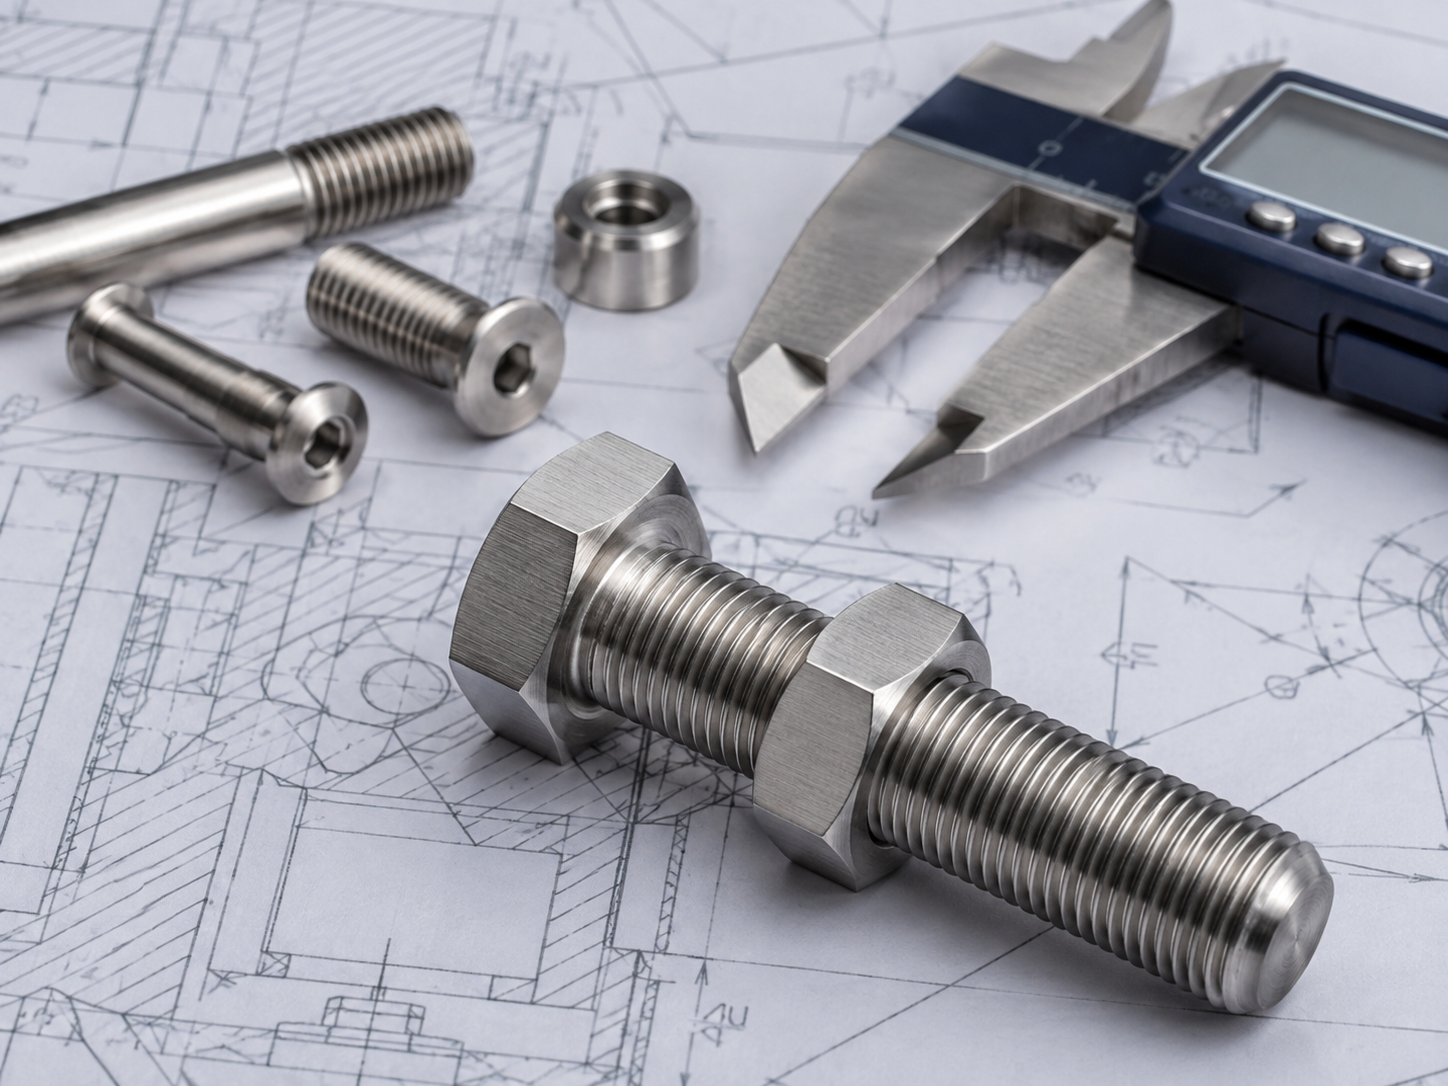
Different grades allow engineers to select the required balance of temperature capability, corrosion resistance and mechanical strength.
304H, 304N, 316Ti, 321, 347 and 347H provide different combinations of elevated-temperature strength, stabilization and corrosion resistance.
Boilers, Heat exchangers, Pressure vessels, High-temperature equipment
Pressure equipment, Structural components, High-load fasteners, Industrial equipment
Chemical processing, Flue gas systems, Heat exchangers, Flanges & valves
Heat exchangers, Furnace components, Exhaust systems, Chemical equipment
Chemical equipment, Expansion joints, Exhaust systems, Flanges & valves
Boilers, Superheaters, Refineries, High-temperature pressure equipment
Additional high-temperature, stabilized and nitrogen-strengthened grades can be reviewed according to project specifications and service requirements.
Compare the principal alloying elements and stabilization mechanisms that influence strength, corrosion resistance and elevated-temperature performance.
| GRADE | C (%) | CR (%) | NI (%) | MO (%) | N (%) | STABILIZING ELEMENT (%) | OTHER (%) |
|---|---|---|---|---|---|---|---|
| 304H / S30409 | 0.04–0.10 | 18.0–20.0 | 8.0–10.5 | — | — | — | Mn 2.00 max, Si 1.00 max |
| 304N / S30451 | 0.08 max | 18.0–20.0 | 8.0–12.0 | — | 0.10–0.16 | — | Mn 2.00 max, Si 1.00 max |
| 316Ti / S31635 | 0.08 max | 16.0–18.0 | 10.0–14.0 | 2.00–3.00 | 0.10 max | Ti: 5×(C+N) min, 0.70 max | Mn 2.00 max, Si 1.00 max |
| 321 / S32100 | 0.08 max | 17.0–19.0 | 9.0–12.0 | — | — | Ti: 5×(C+N) min, 0.70 max | Mn 2.00 max, Si 1.00 max |
| 347 / S34700 | 0.08 max | 17.0–19.0 | 9.0–12.0 | — | — | Nb: 10×C min, 1.10 max | Mn 2.00 max, Si 1.00 max |
| 347H / S34709 | 0.04–0.10 | 17.0–19.0 | 9.0–12.0 | — | — | Nb: 8×C min, 1.10 max | Mn 2.00 max, Si 1.00 max |
Reference values are provided for general comparison only. The governing material specification and batch MTC take precedence for production and acceptance.
These grades provide different combinations of room-temperature strength, ductility and elevated-temperature performance according to their alloy design.
| GRADE / CONDITION | TENSILE STRENGTH (MPa) | 0.2% YIELD STRENGTH (MPa) | ELONGATION (%) |
|---|---|---|---|
| 304H — Annealed Bar Reference | 515 min | 205 min | 30 min |
| 304N — Annealed Bar Reference | 550 min | 240 min | 30 min |
| 316Ti — Annealed Bar Reference | 515 min | 205 min | 30 min |
| 321 — Annealed Bar Reference | 515 min | 205 min | 30 min |
| 347 — Annealed Bar Reference | 515 min | 205 min | 30 min |
| 347H — Annealed Bar Reference | 515 min | 205 min | 30 min |
Mechanical properties depend on product form, dimensions, material condition, heat treatment and the applicable specification. The purchase specification and actual inspection certificate shall govern the order.
Choose the grade according to temperature, stabilization method, corrosion environment and required mechanical strength.
| Application Requirement | Recommended Grade |
|---|---|
| General elevated-temperature service | 304H |
| Improved creep strength in a 304-type composition | 304H |
| Higher yield strength through nitrogen alloying | 304N |
| Nitrogen-strengthened pressure equipment | 304N |
| Molybdenum alloying with titanium stabilization | 316Ti |
| Chloride exposure with stabilization required | 316Ti |
| Titanium-stabilized high-temperature service | 321 |
| Niobium-stabilized corrosion resistance | 347 |
| Elevated-temperature niobium-stabilized service | 347H |
| Boilers, superheaters and refinery equipment | 347H |
| Severe chloride or highly corrosive service | Evaluate Duplex, Super Duplex or Super Austenitic grades |
Specialized stainless steel fasteners are available in standard and custom configurations for thermal, chemical, pressure-equipment and industrial applications.
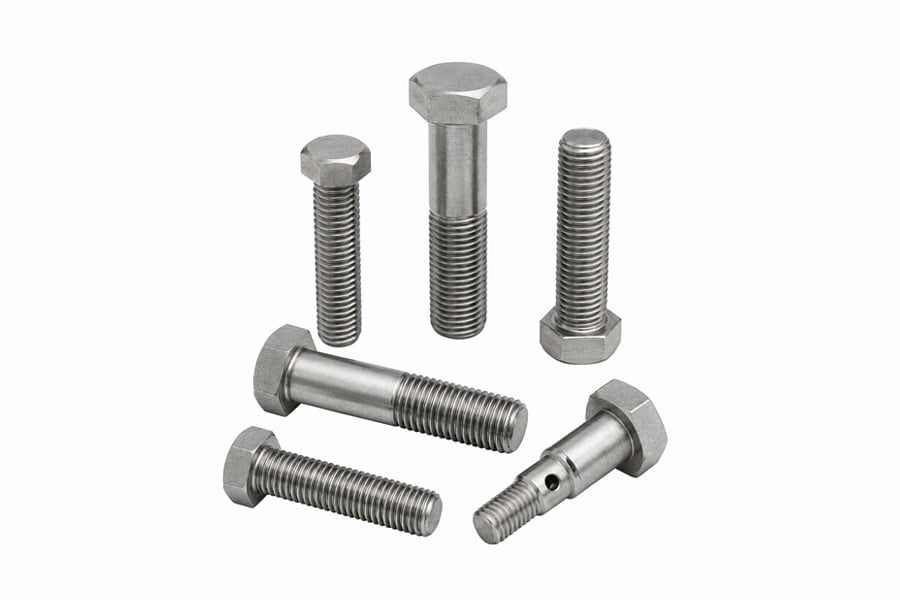
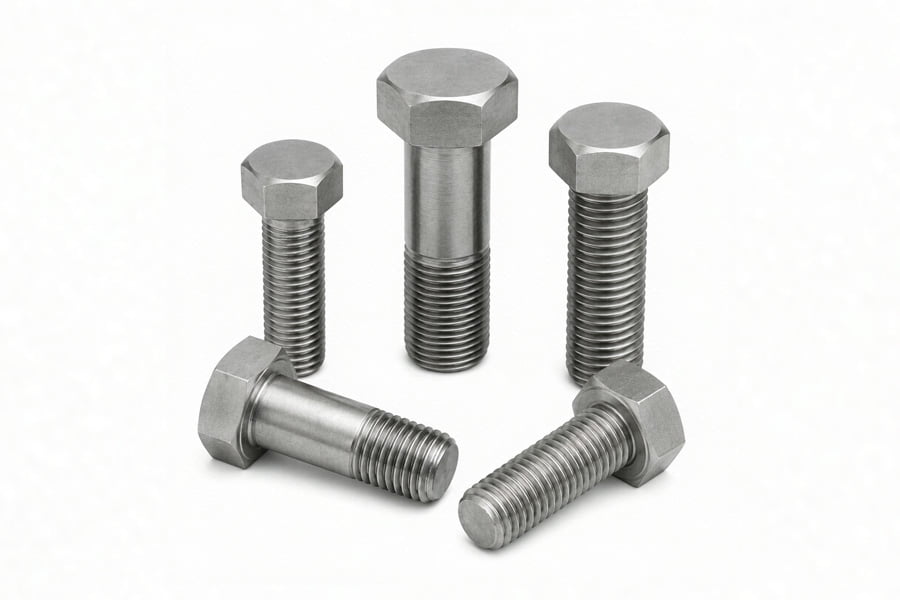
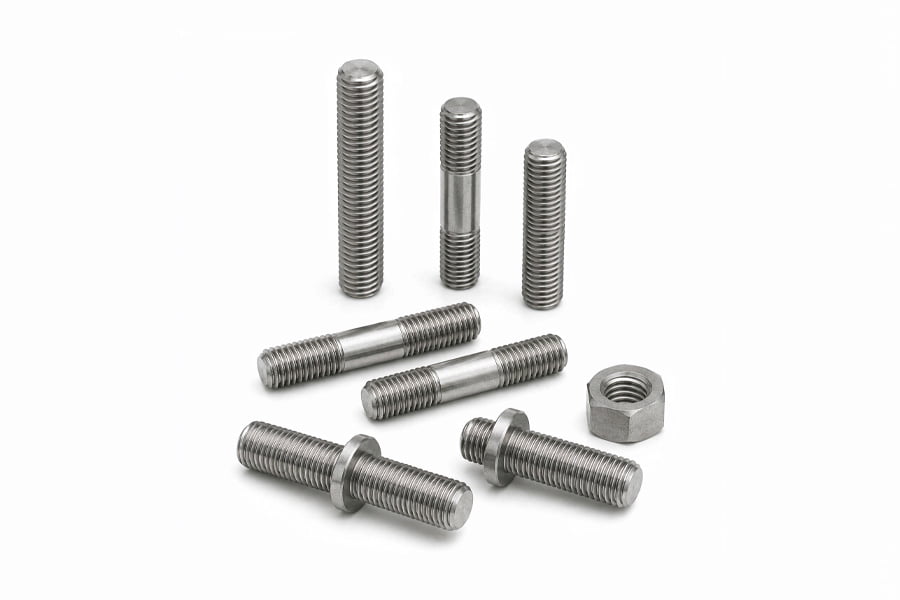
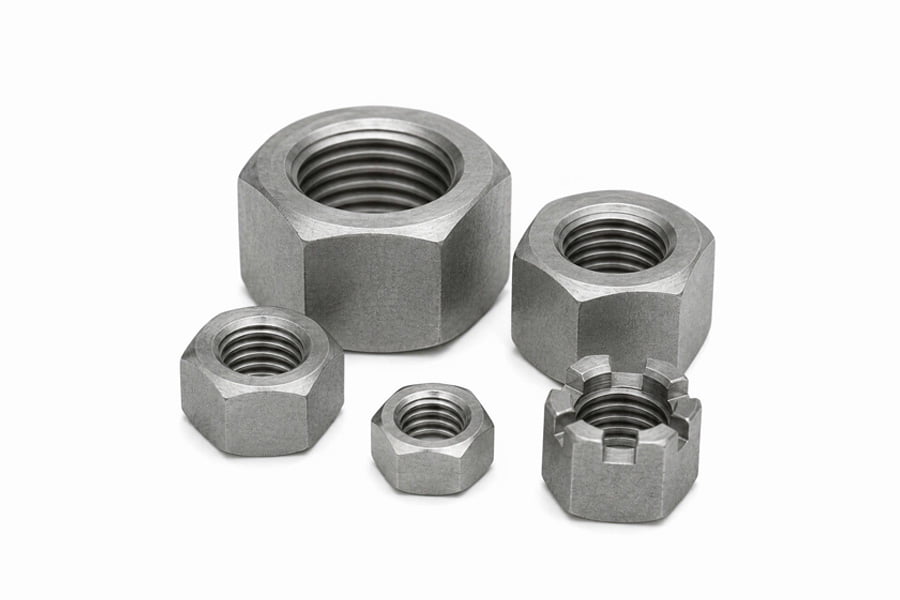
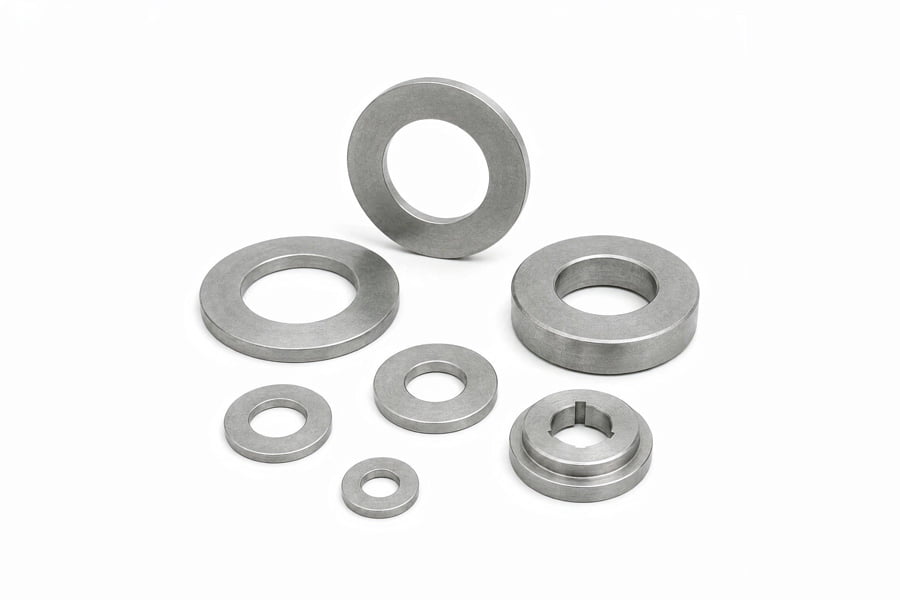
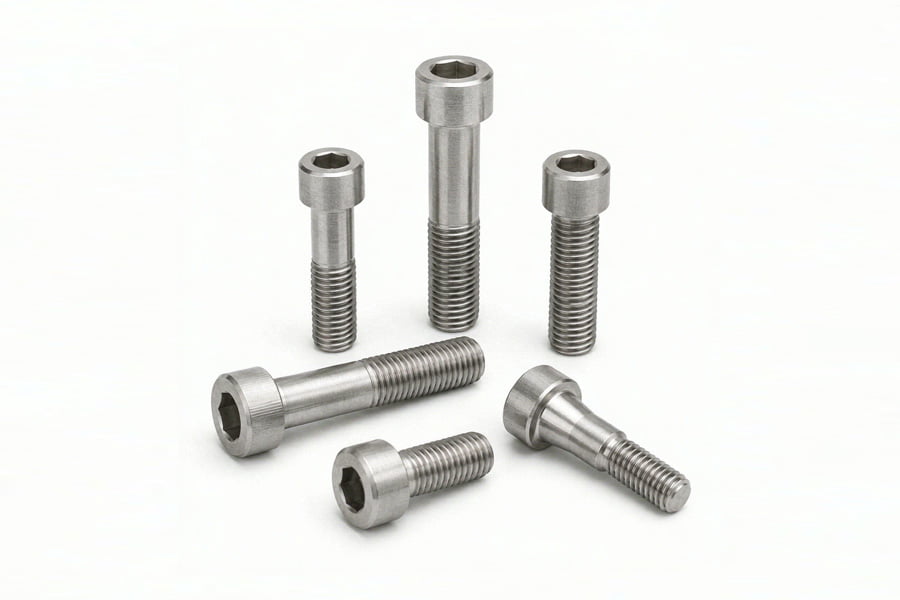
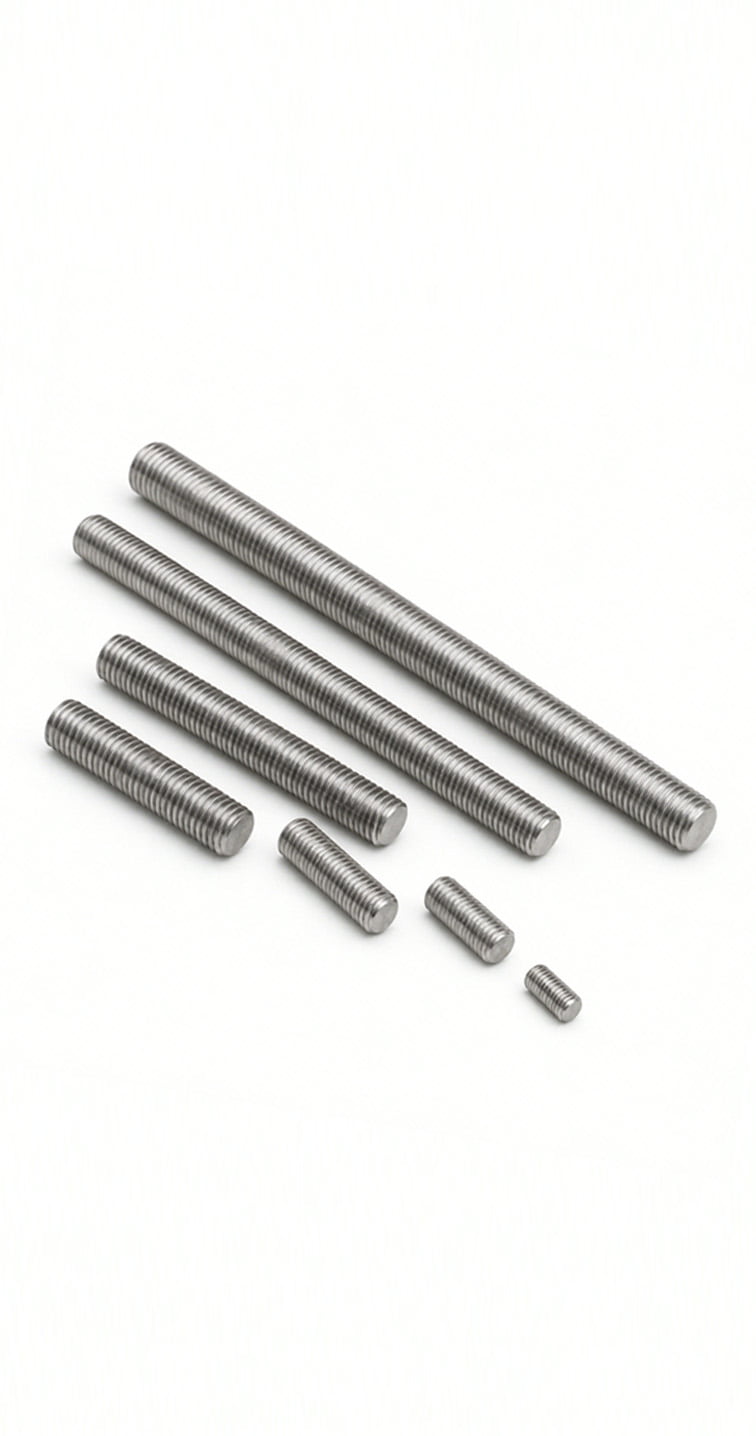
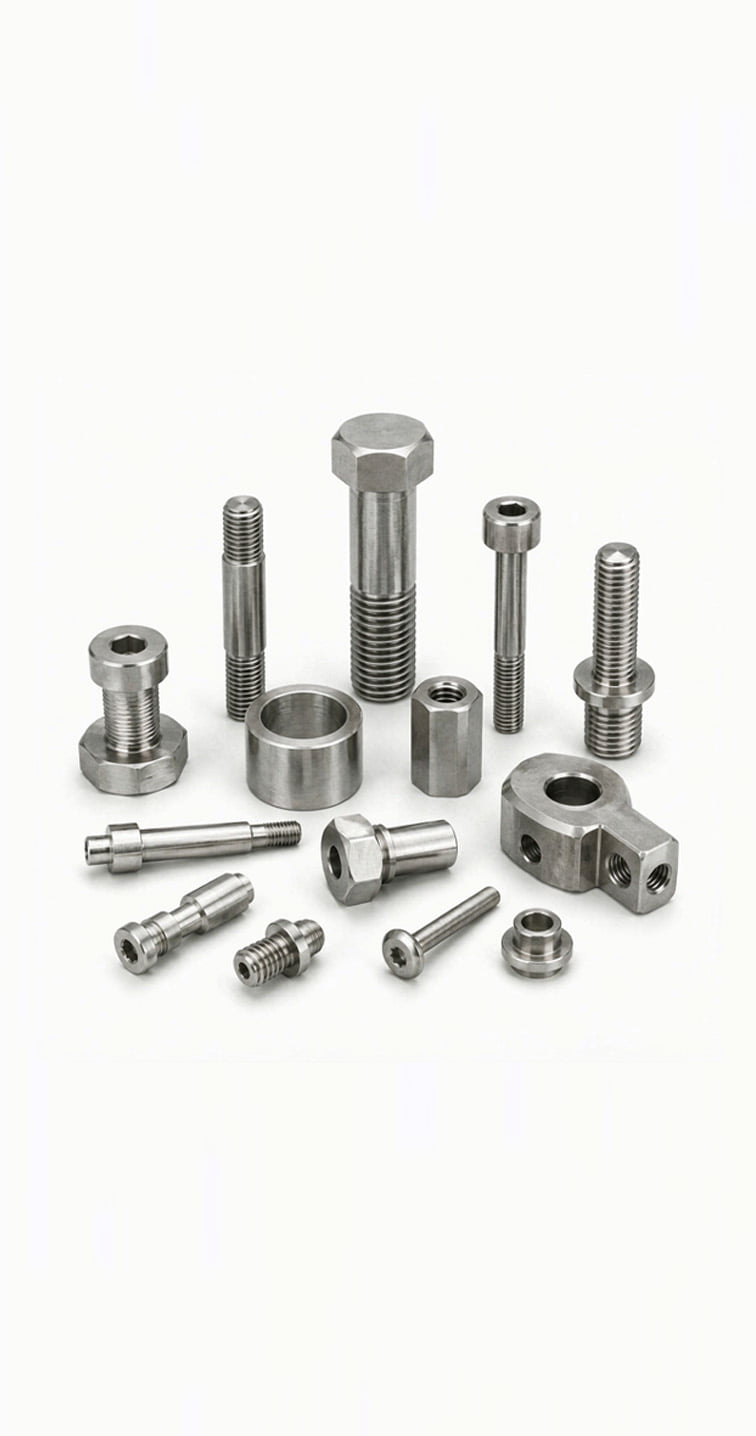
We also manufacture custom and project-specific fasteners according to drawings, specifications or application requirements.
A controlled six-stage production workflow supports consistent manufacturing from reviewed raw material to finished, identified and export-ready specialty-alloy fasteners.
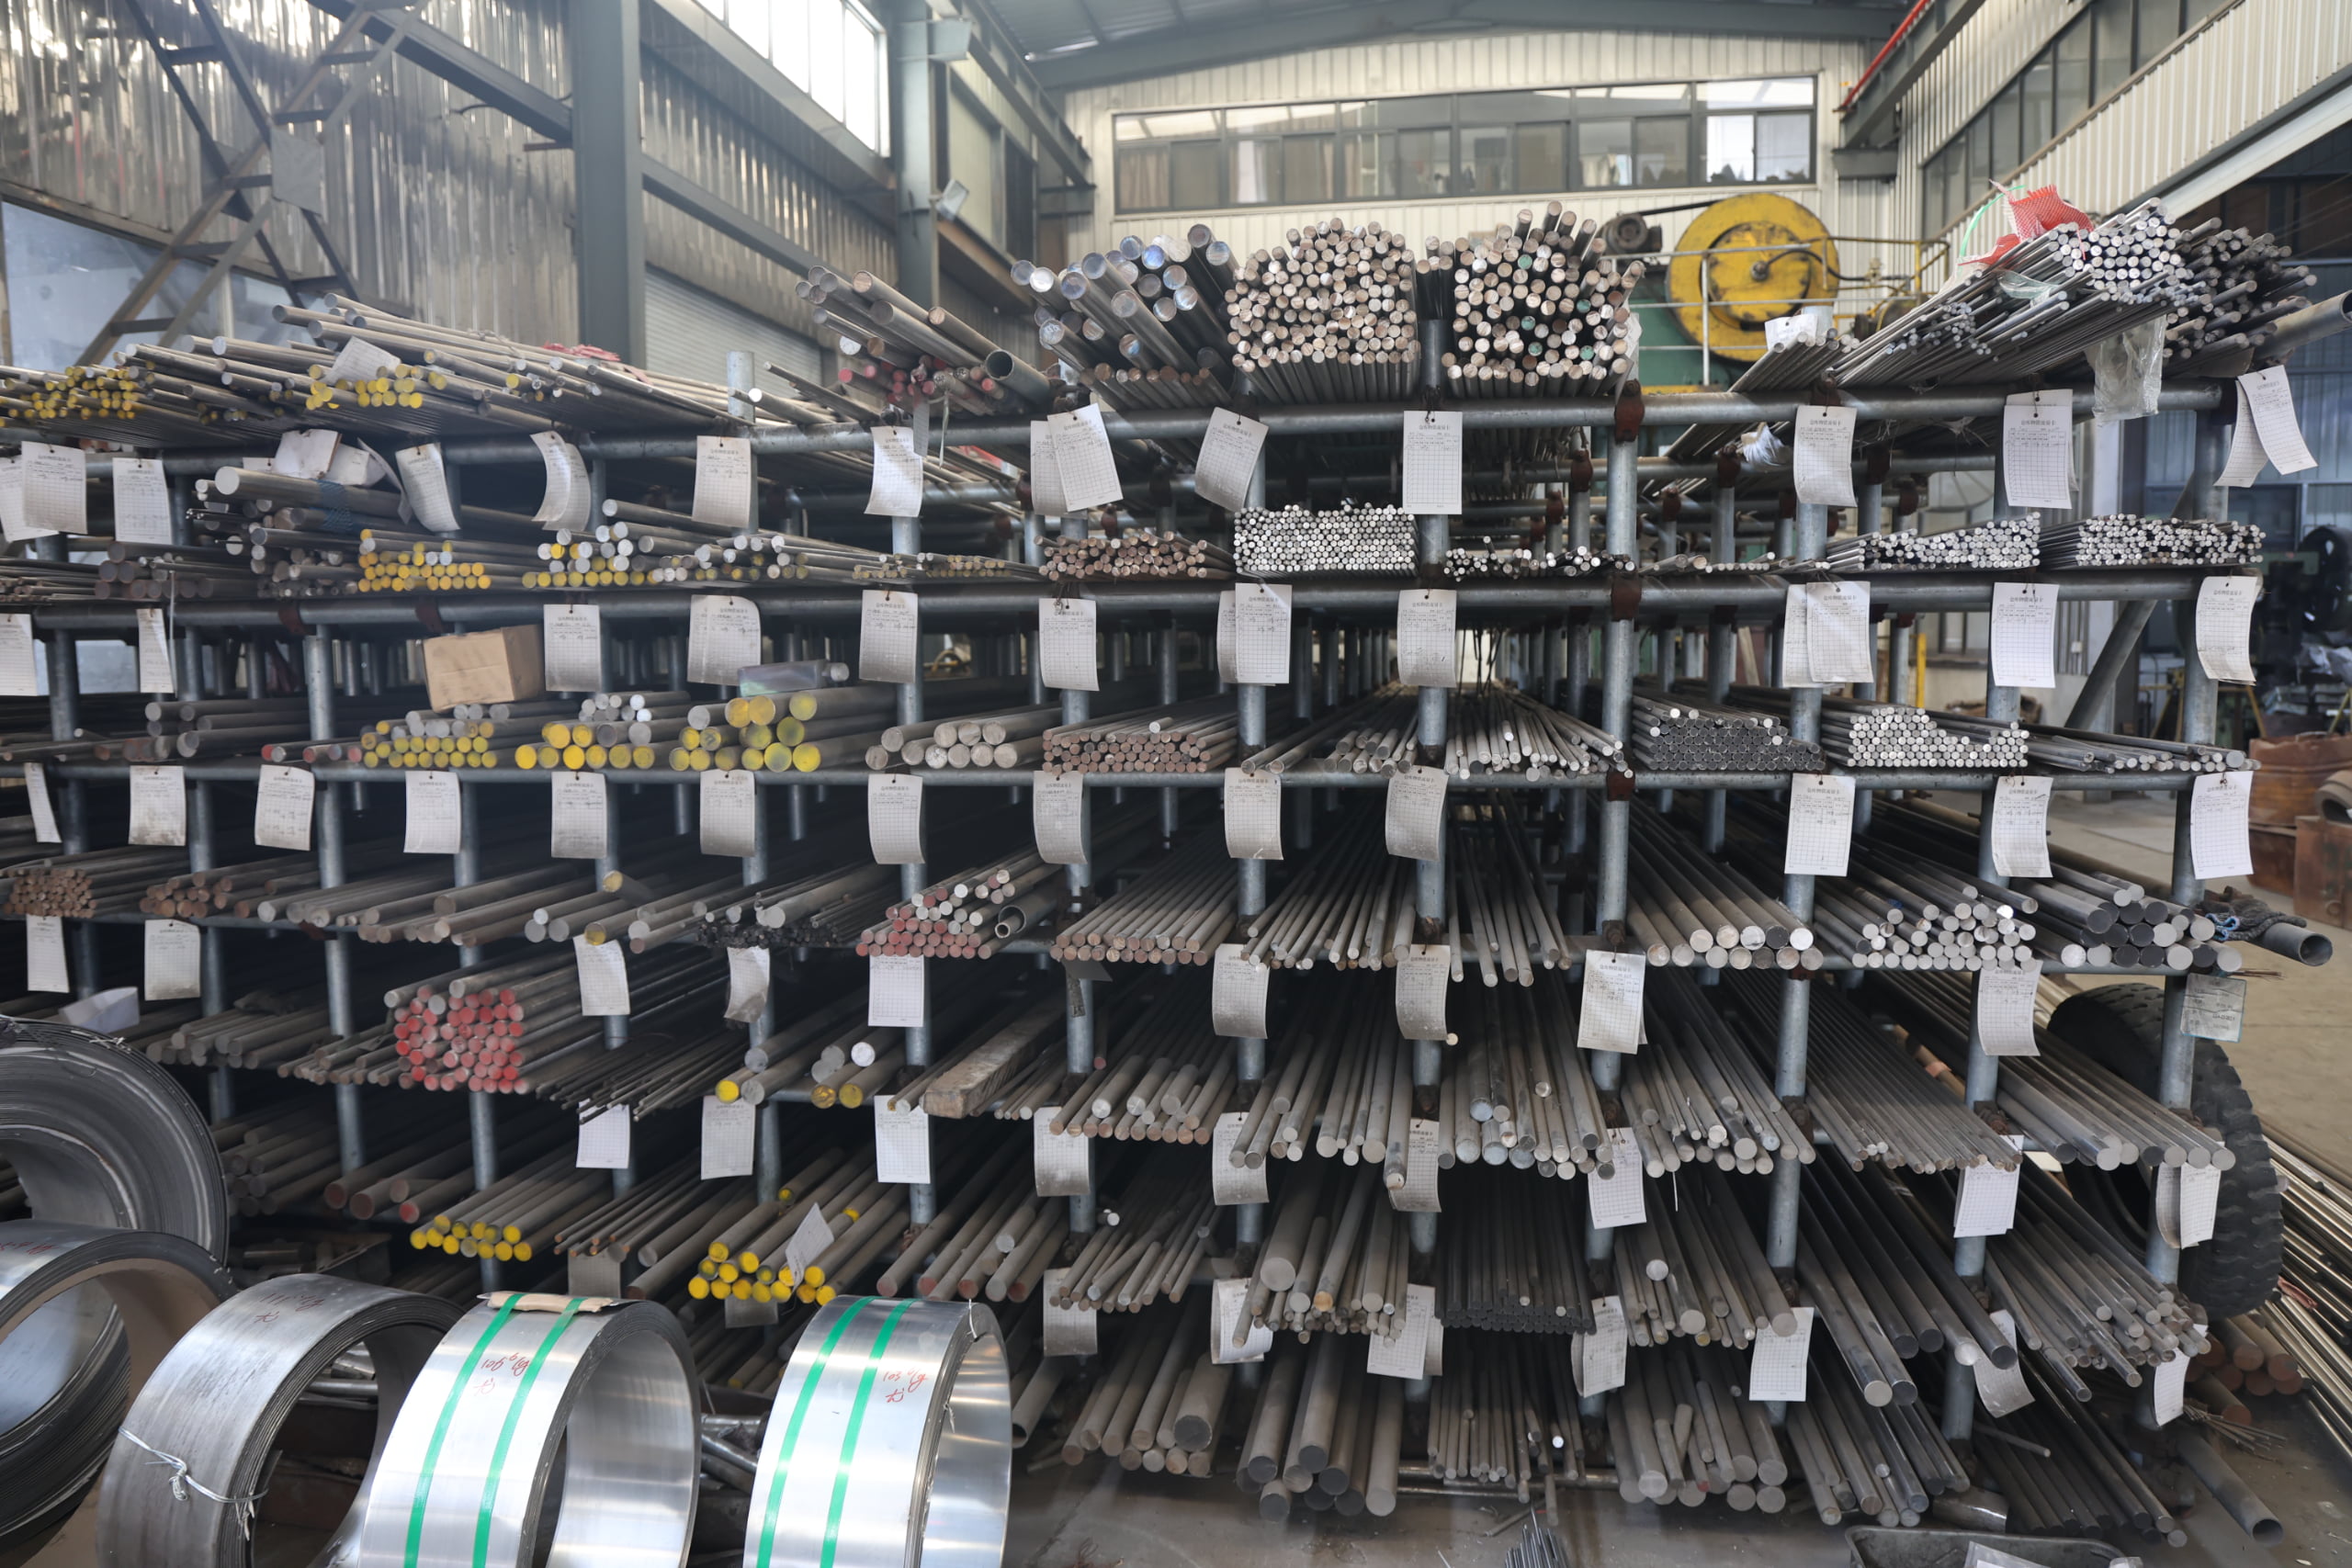
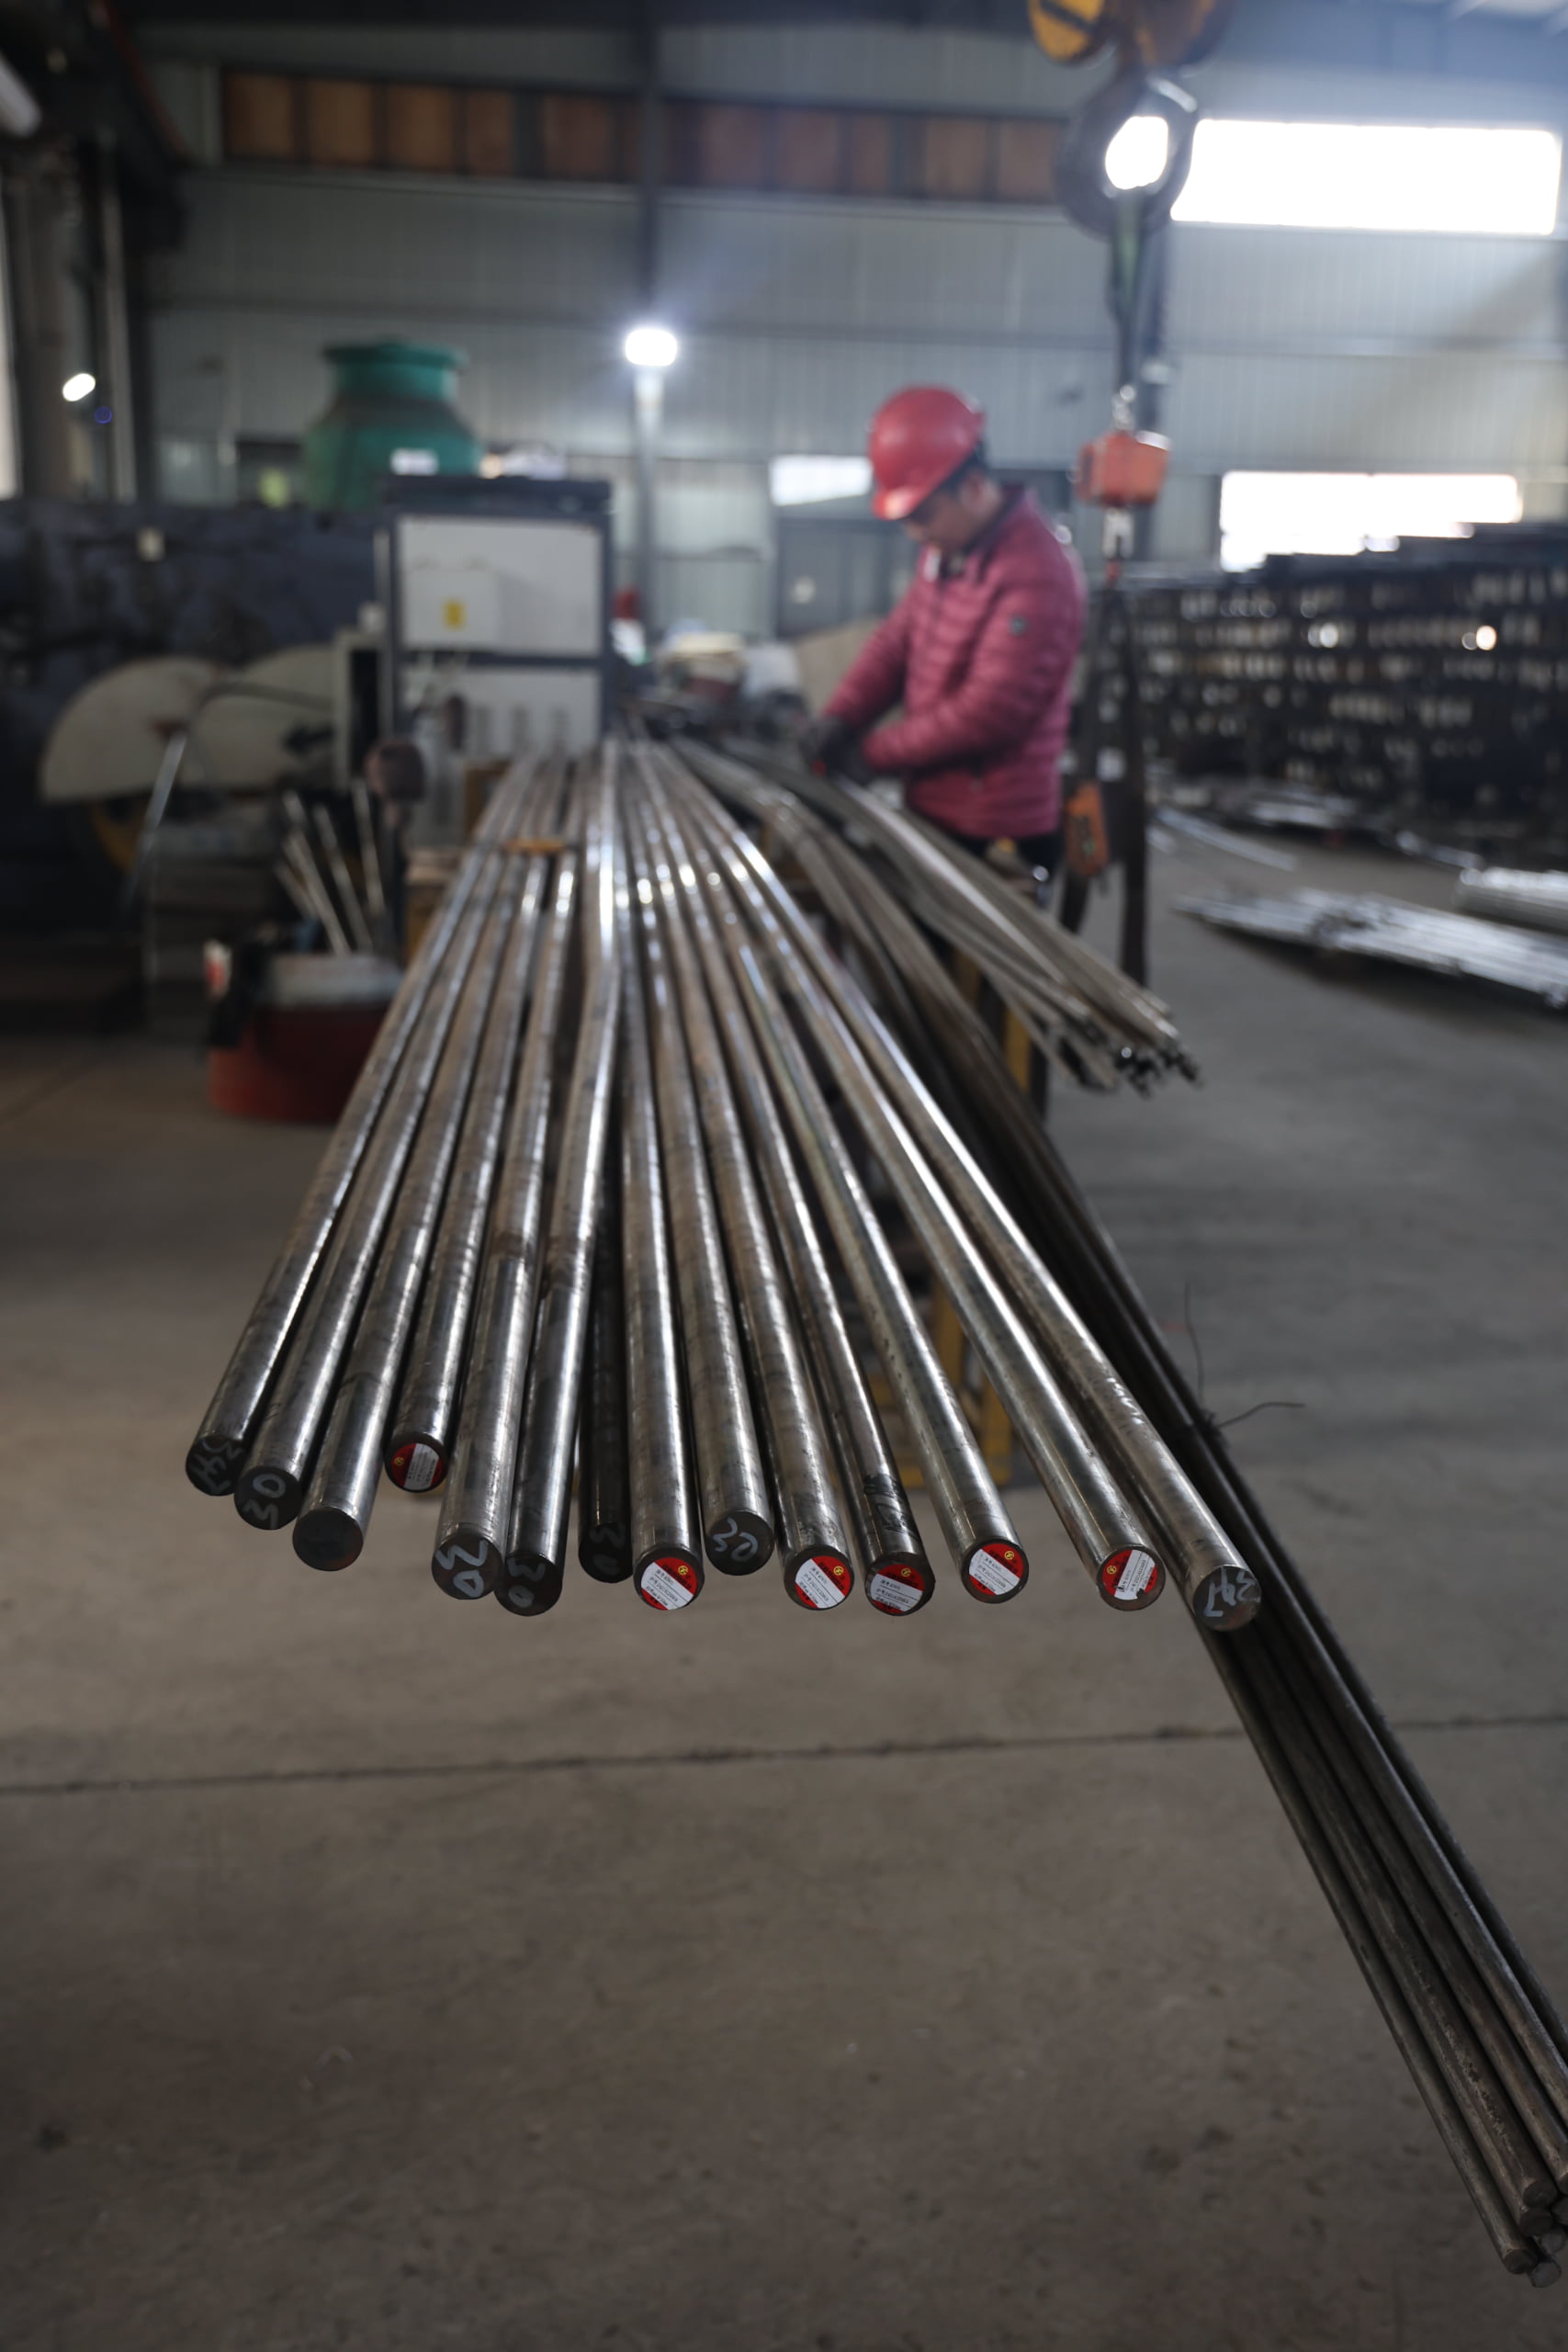
The specified alloy grade, product form, material condition and batch identity are reviewed before cutting. Stock is prepared according to the order and selected manufacturing route.
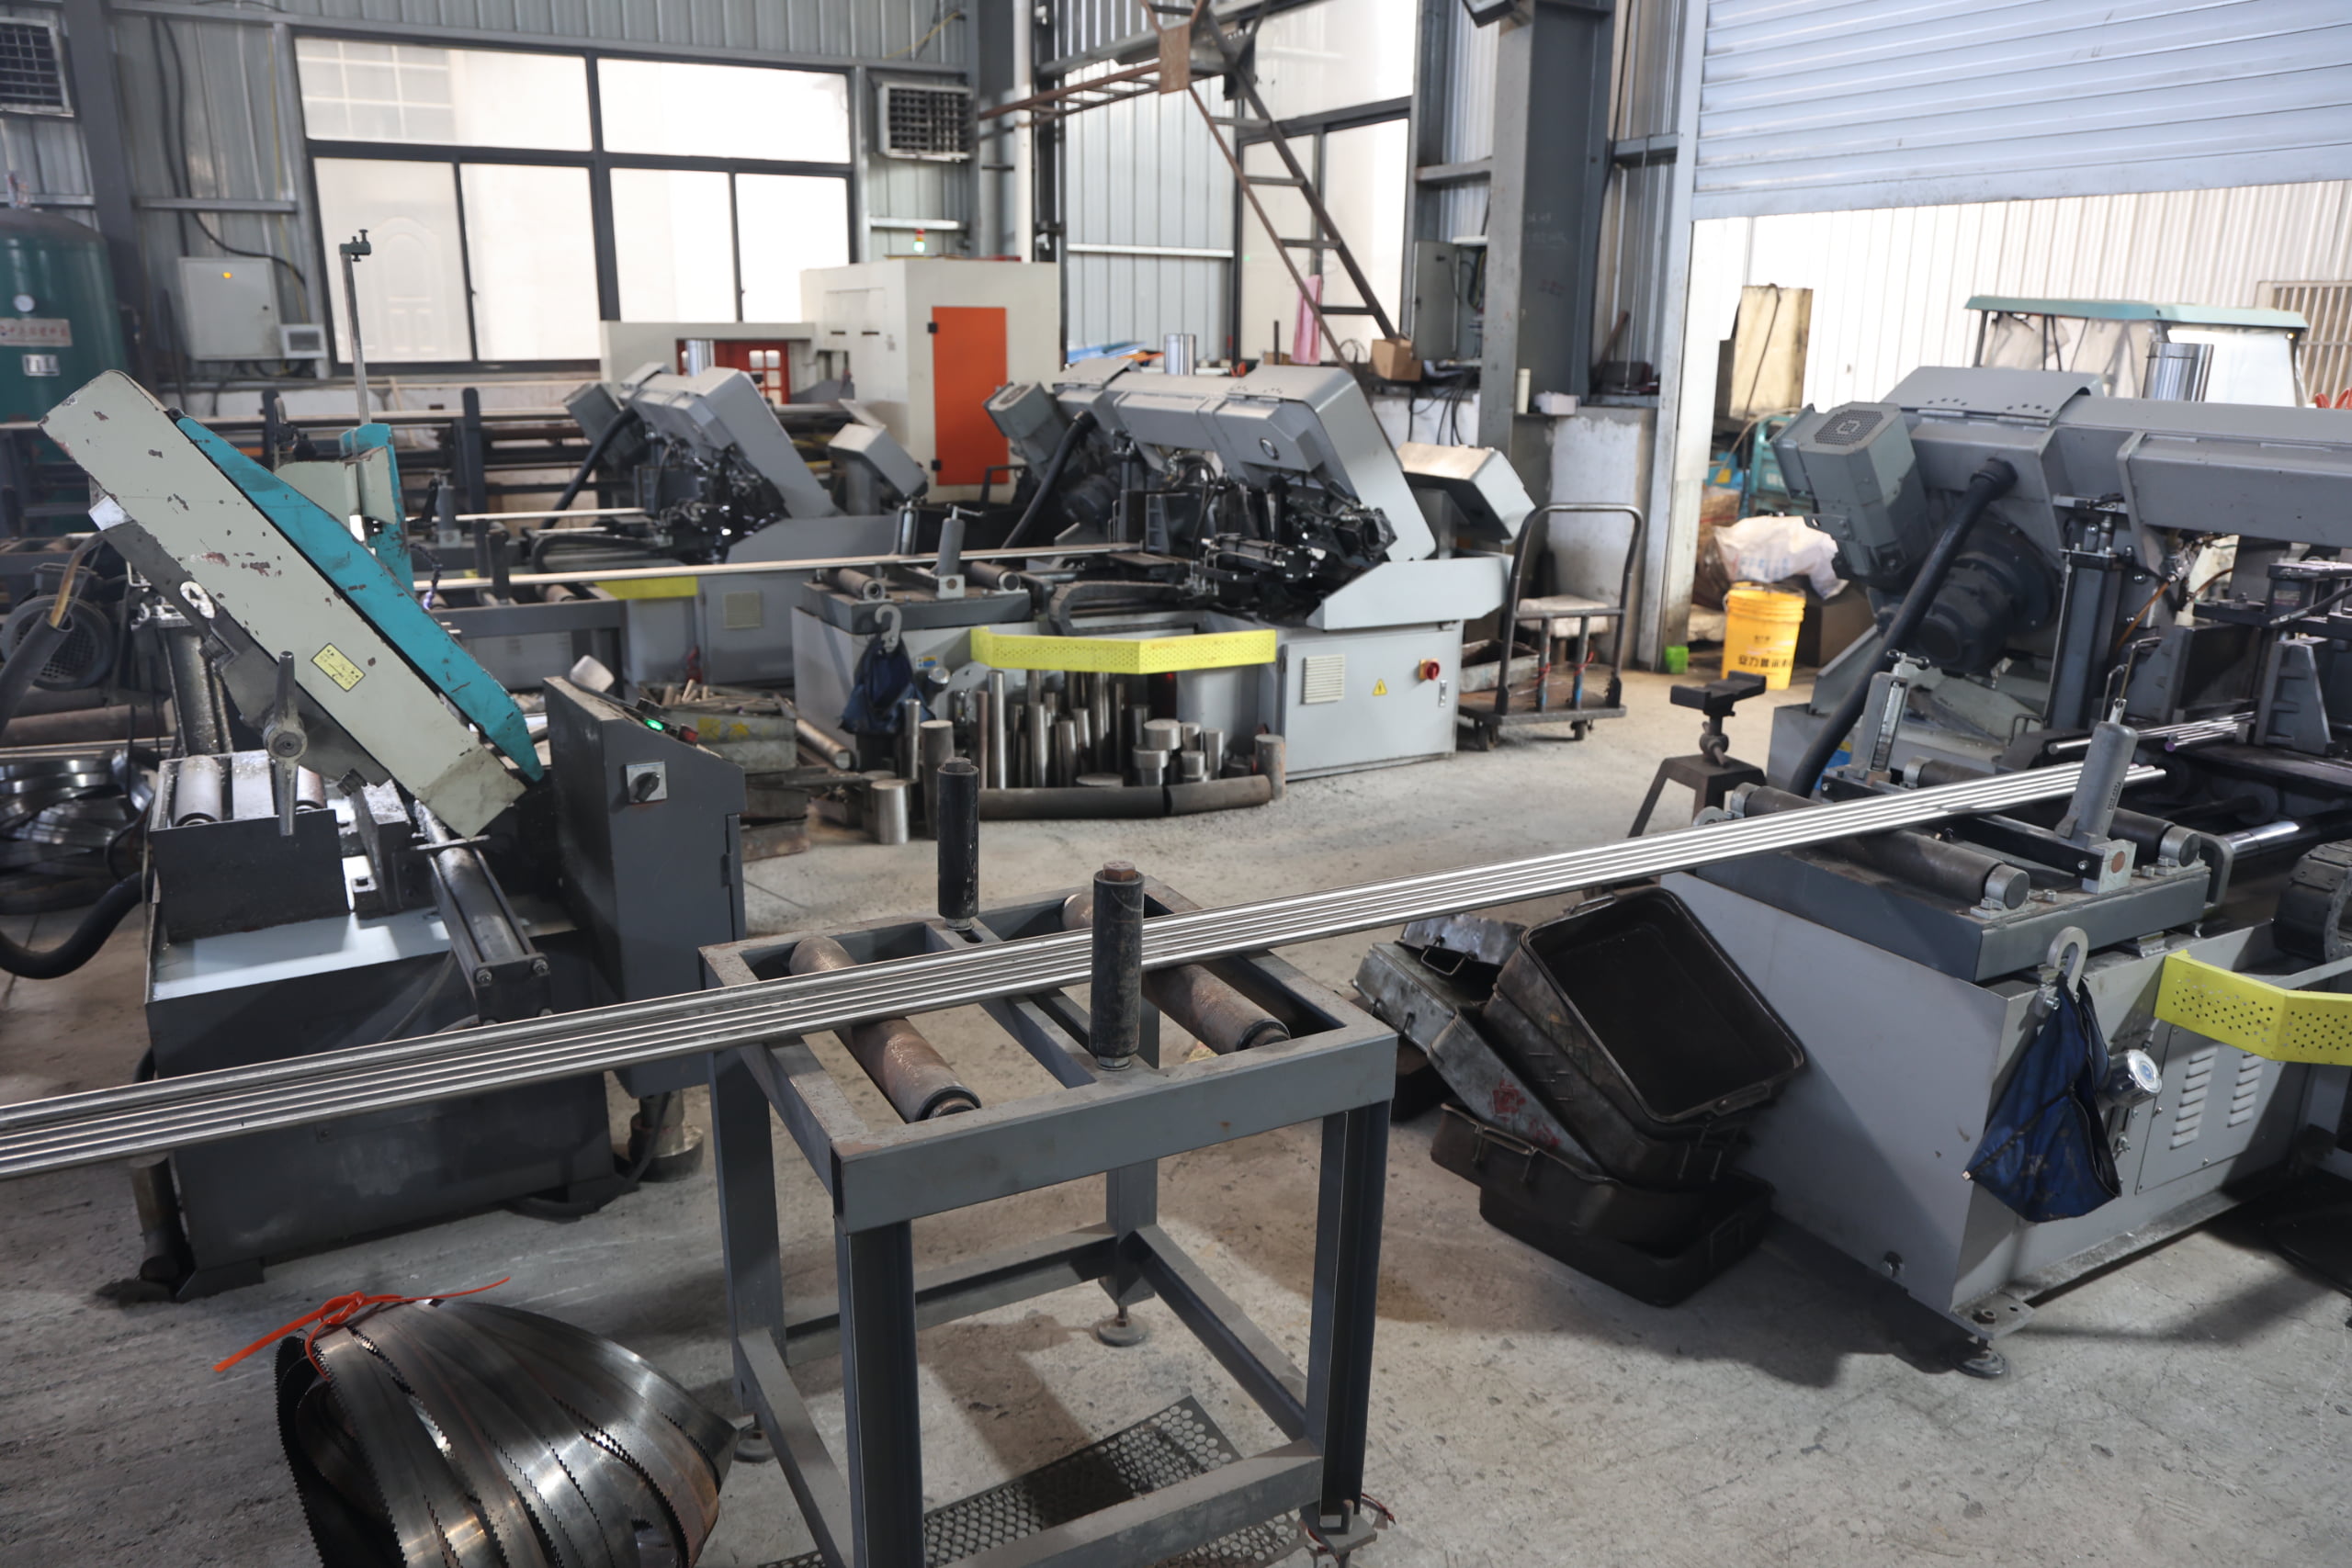
Bars, rods or forgings are cut to the required blank size while maintaining material separation and batch identification.
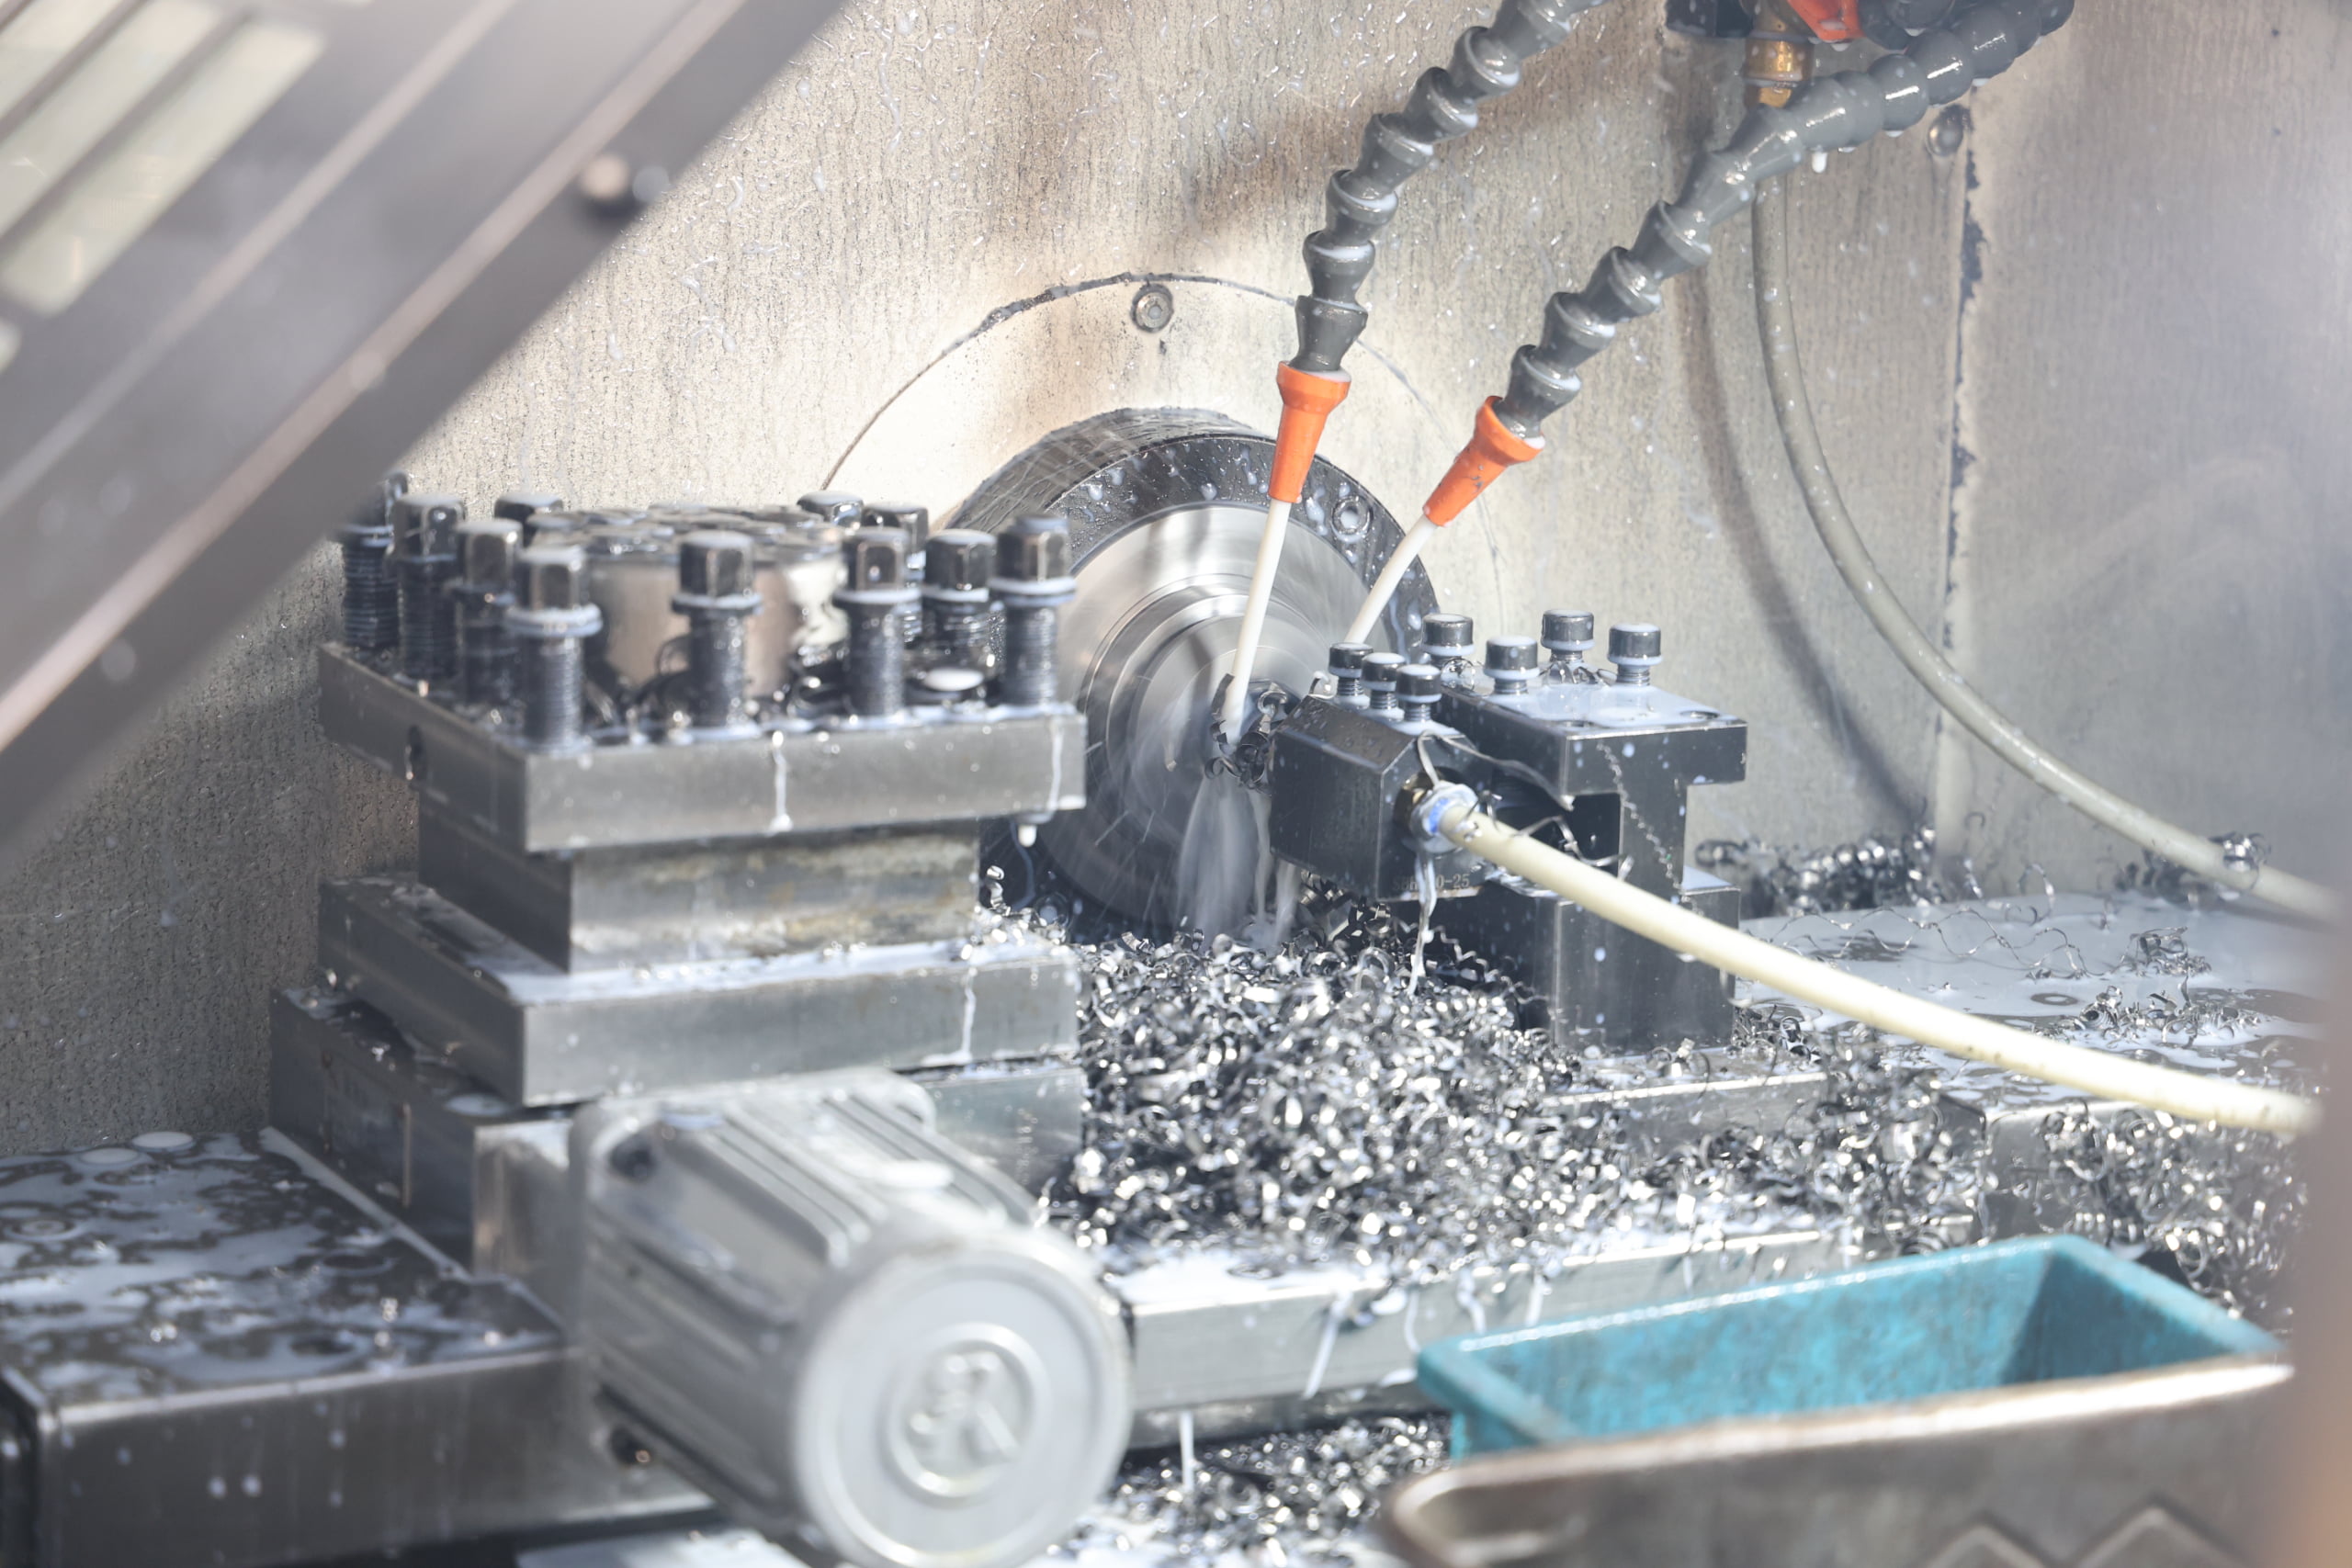
Headed fasteners are forged and machined when appropriate, while complex, low-volume or drawing-based components can be produced by precision CNC machining.
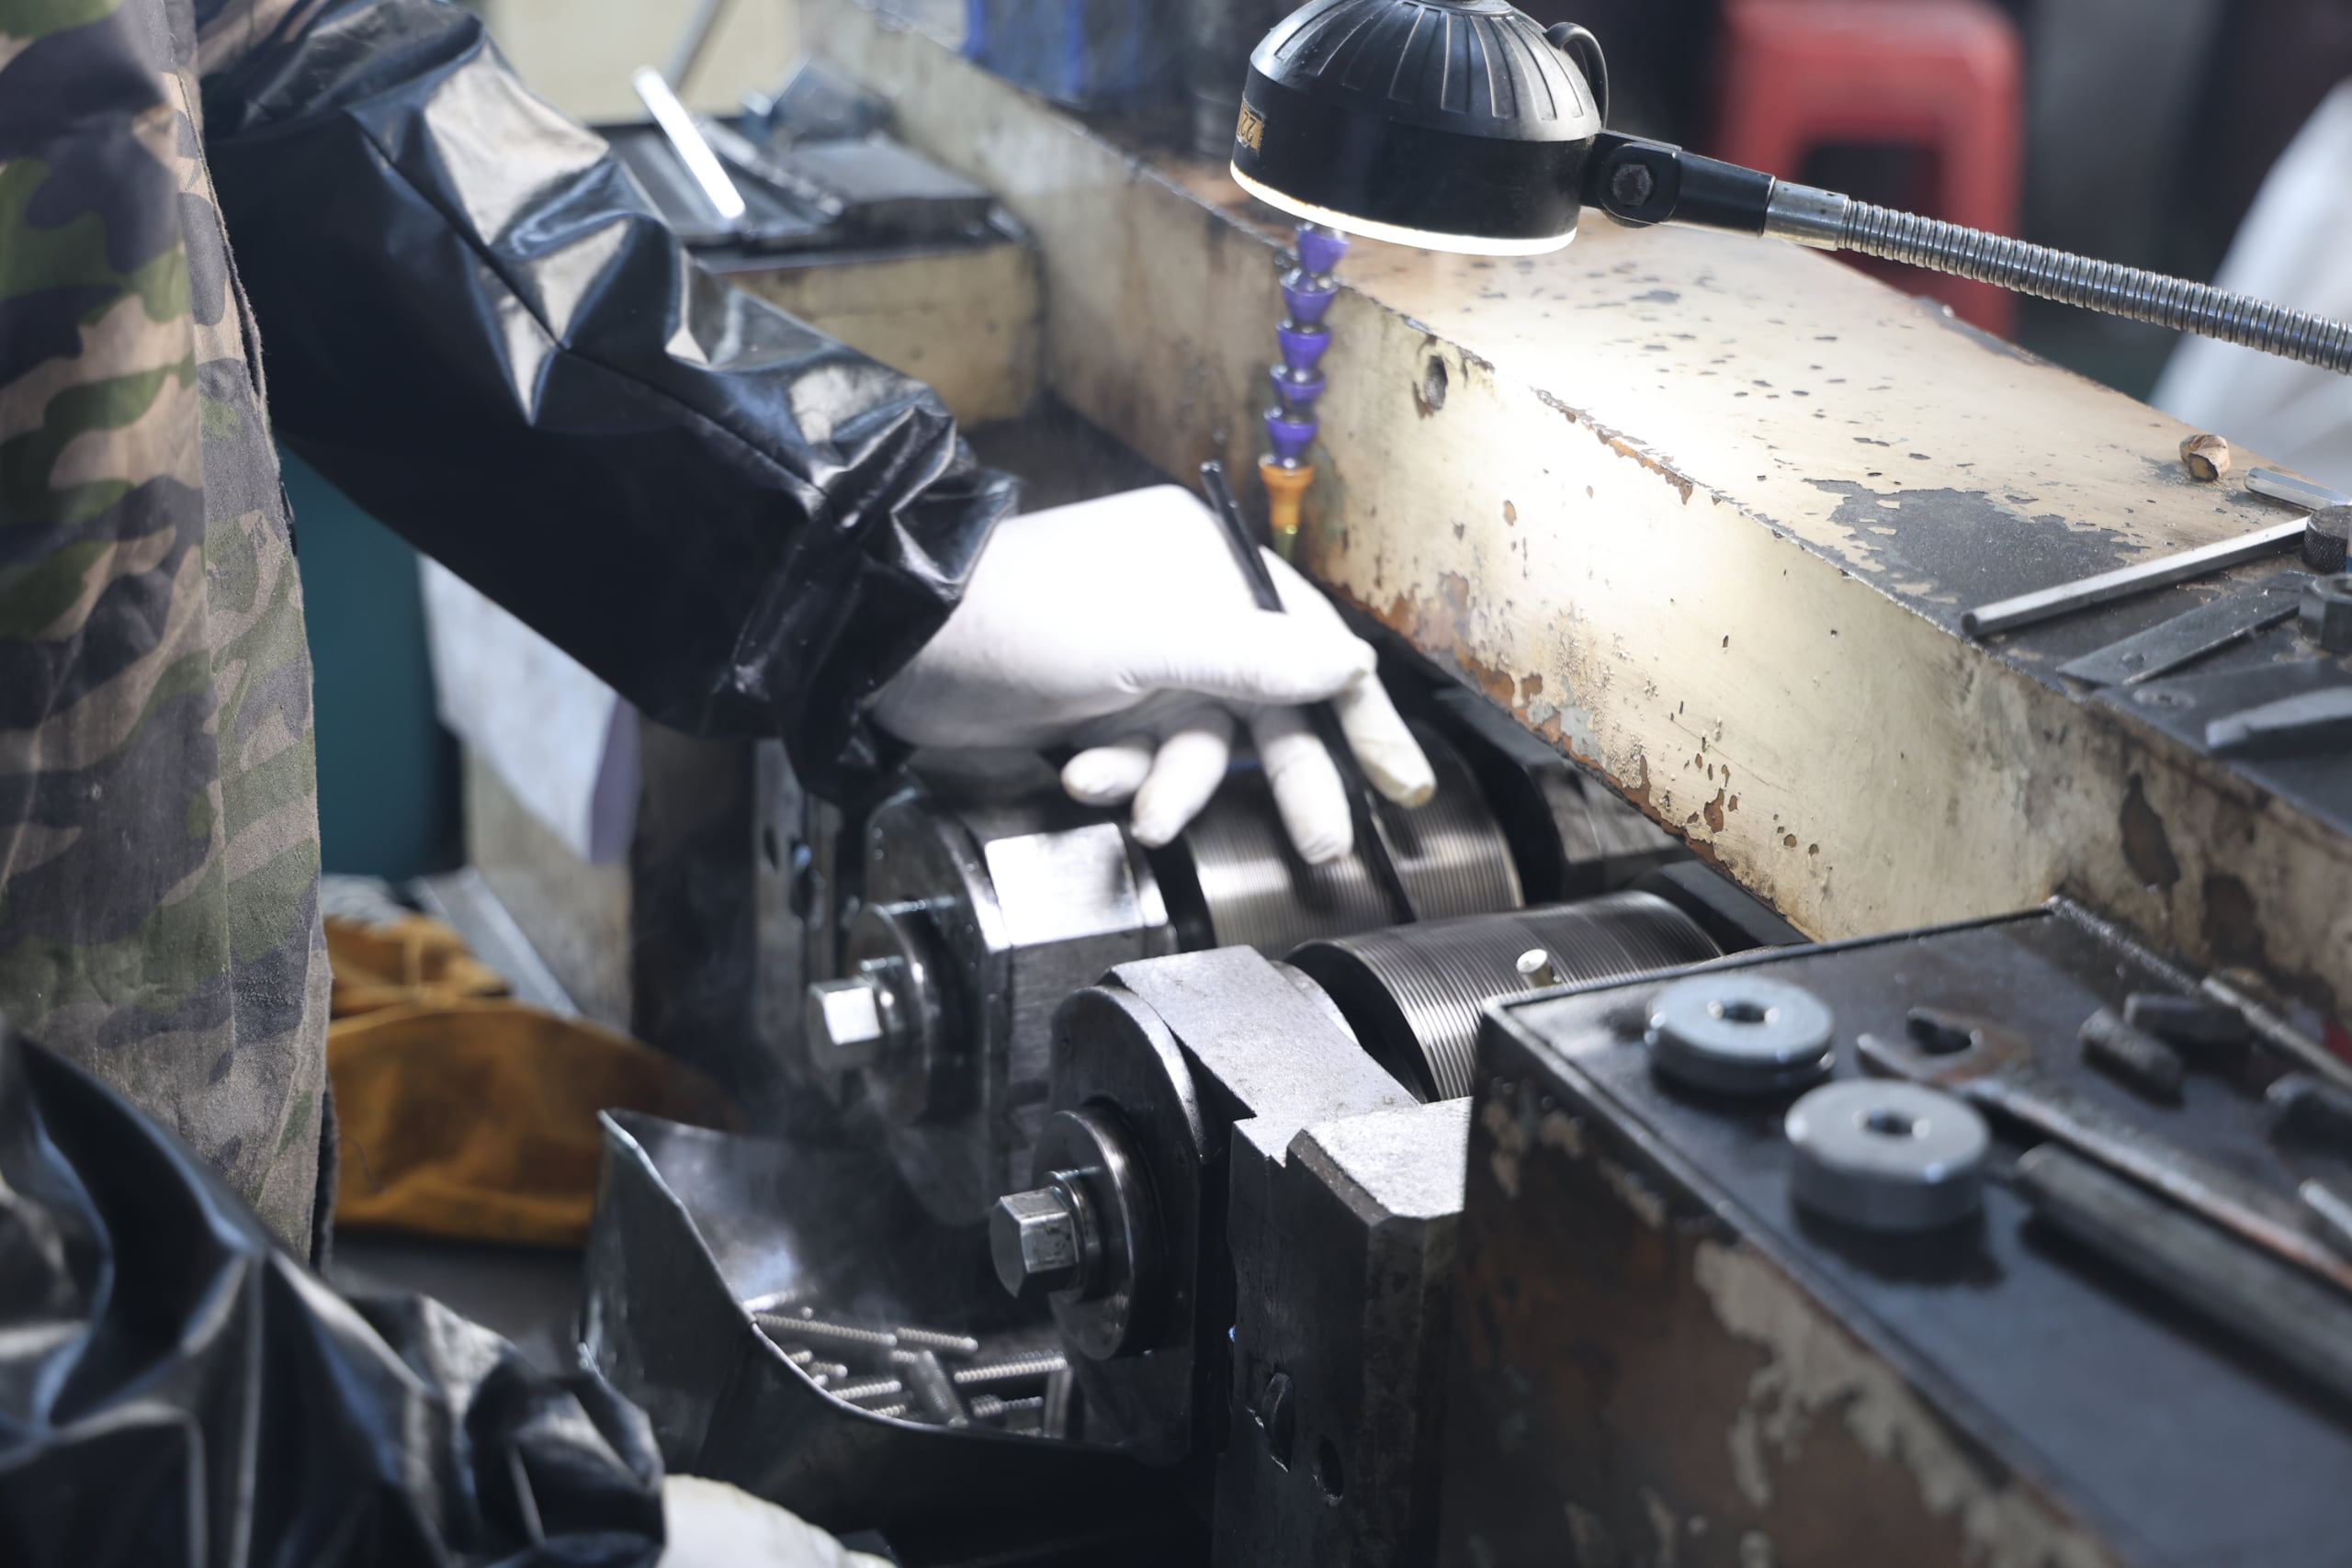
Threads are rolled or cut according to material condition, product geometry, dimensional standard and customer requirements.
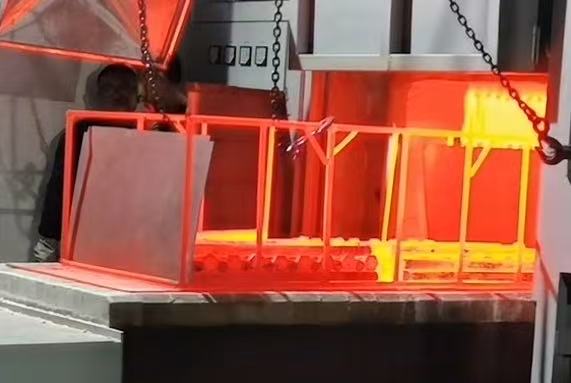
Solution treatment, annealing, age hardening or other thermal processing is applied only when required by the alloy grade, material condition and governing specification.
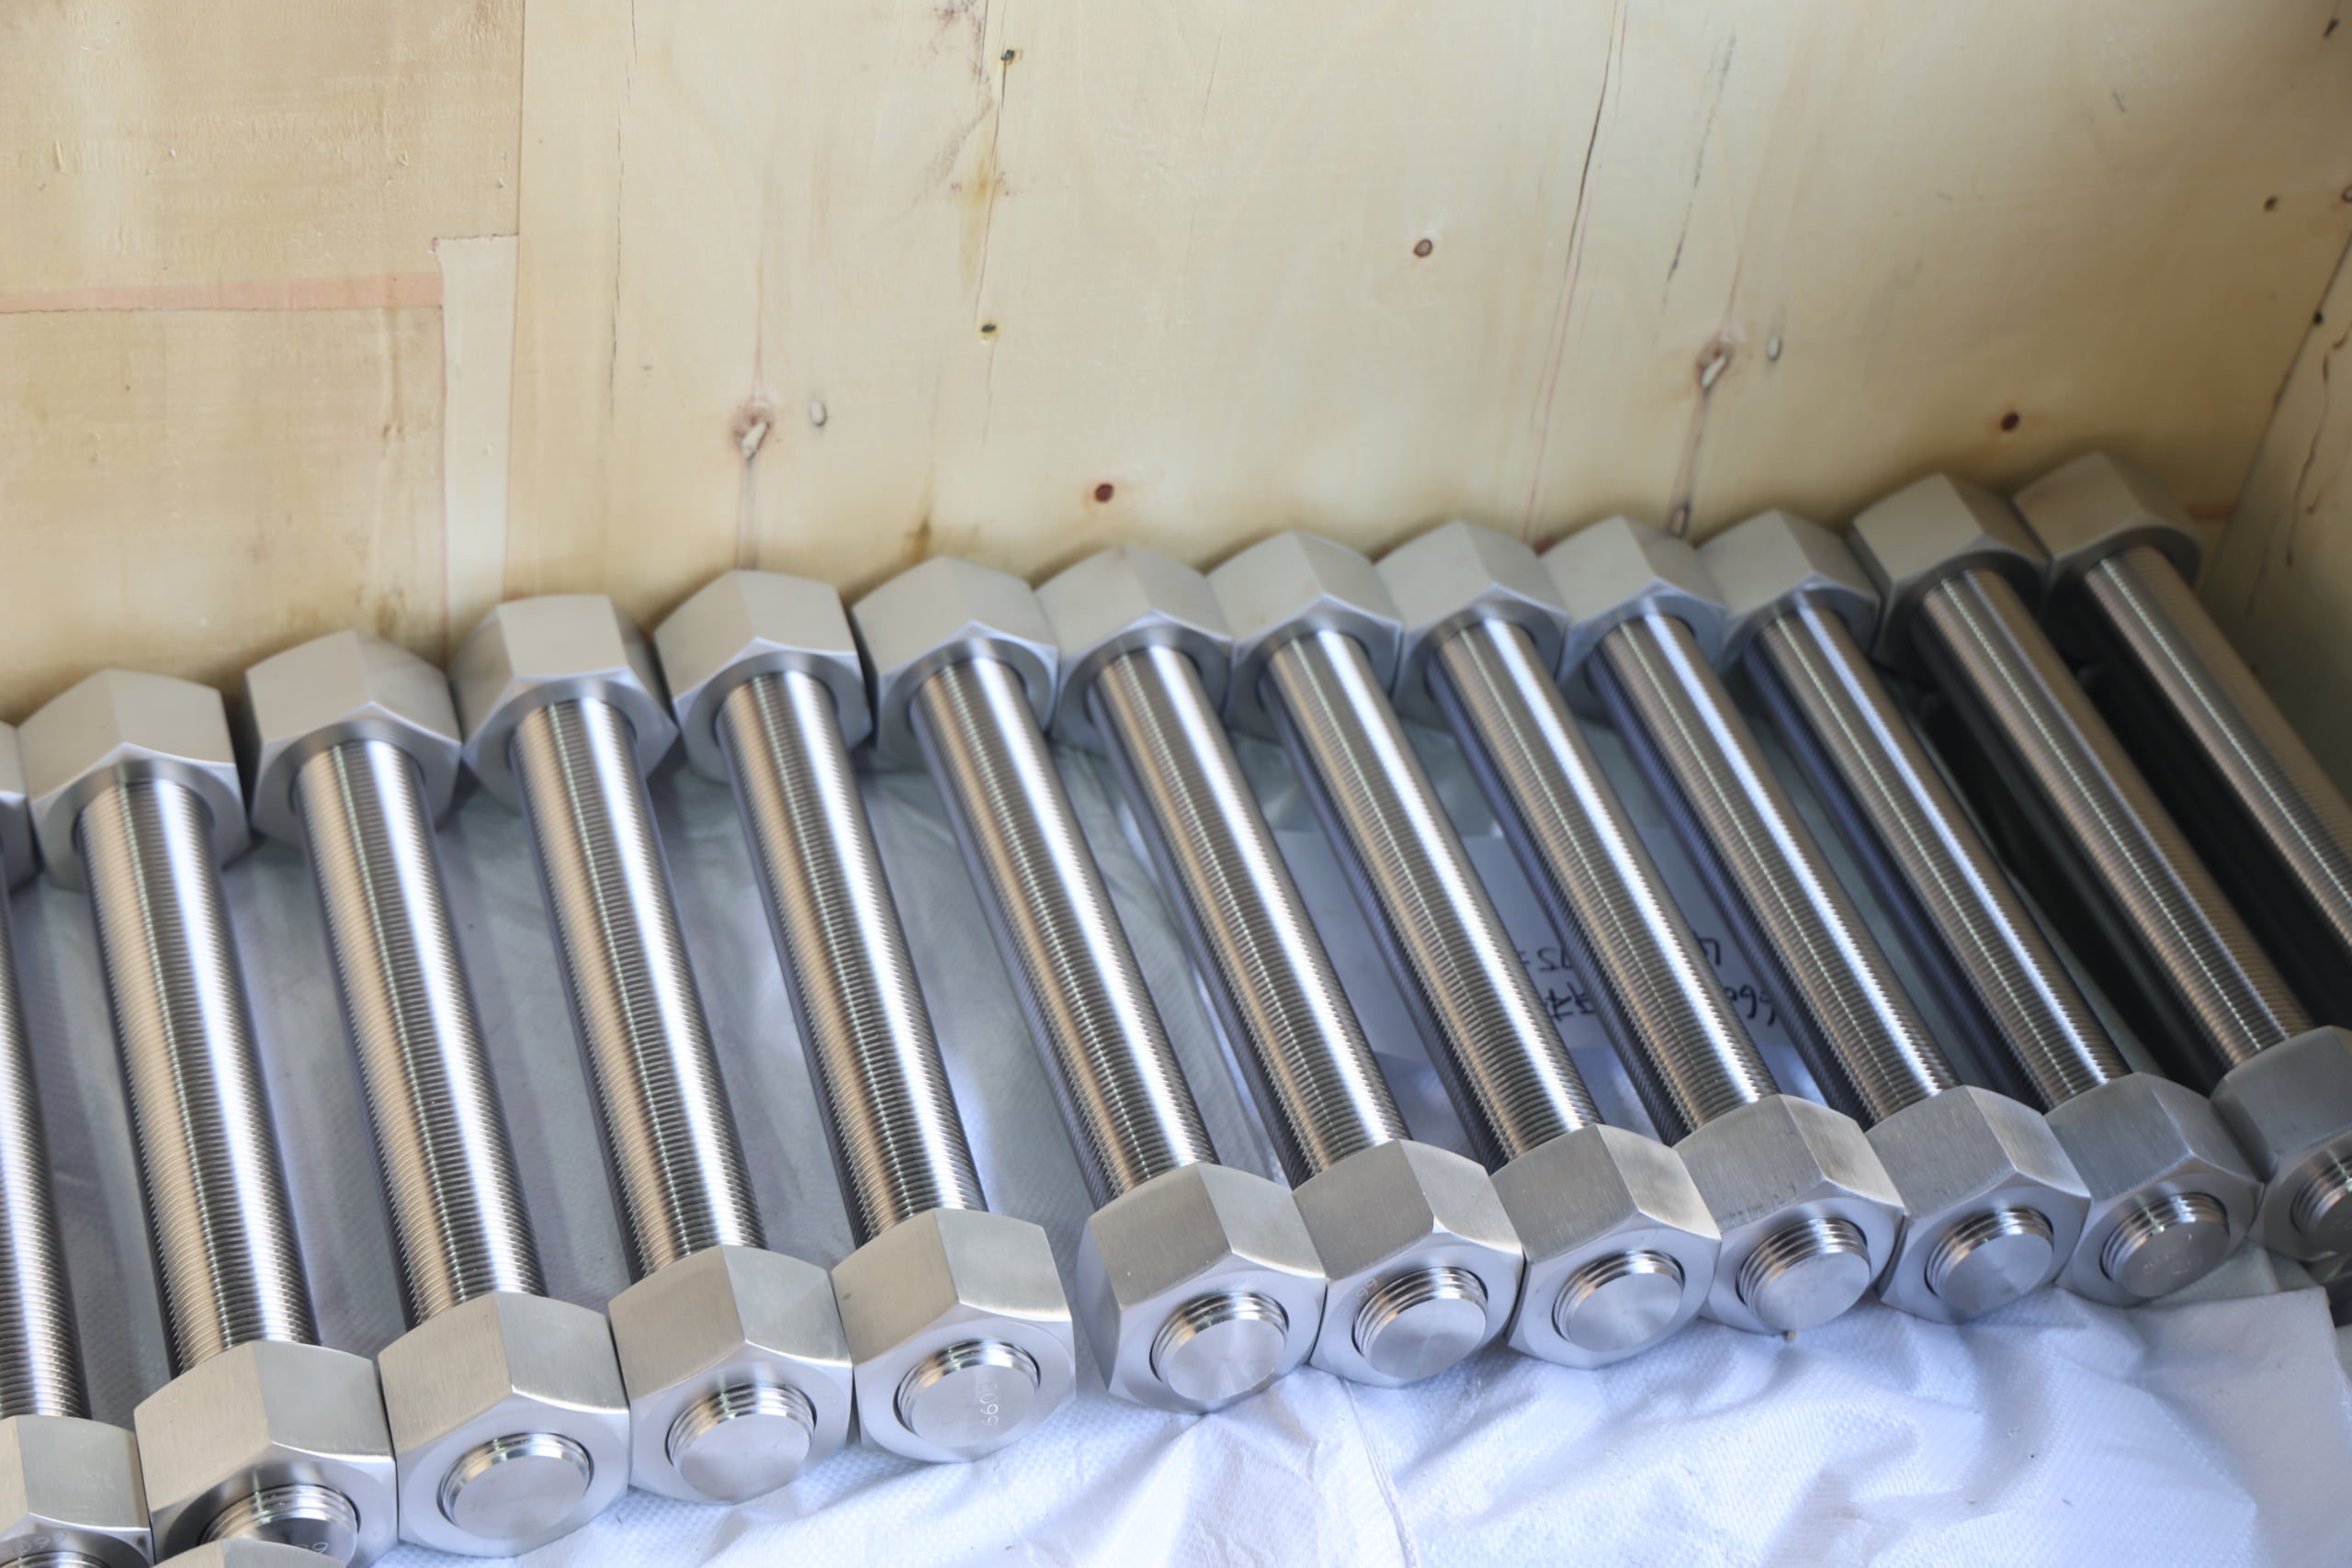
Finished parts are deburred, cleaned and prepared as specified, then identified and packed according to order and traceability requirements.
Inspection and documentation are planned around the purchase specification, customer drawing and intended service. The agreed inspection scope is confirmed according to individual project requirements.
Material grade, heat or lot number and incoming documents are checked against the agreed order requirements before production.
Batch identity is maintained through production, inspection and packing so finished parts can be linked to their source material.
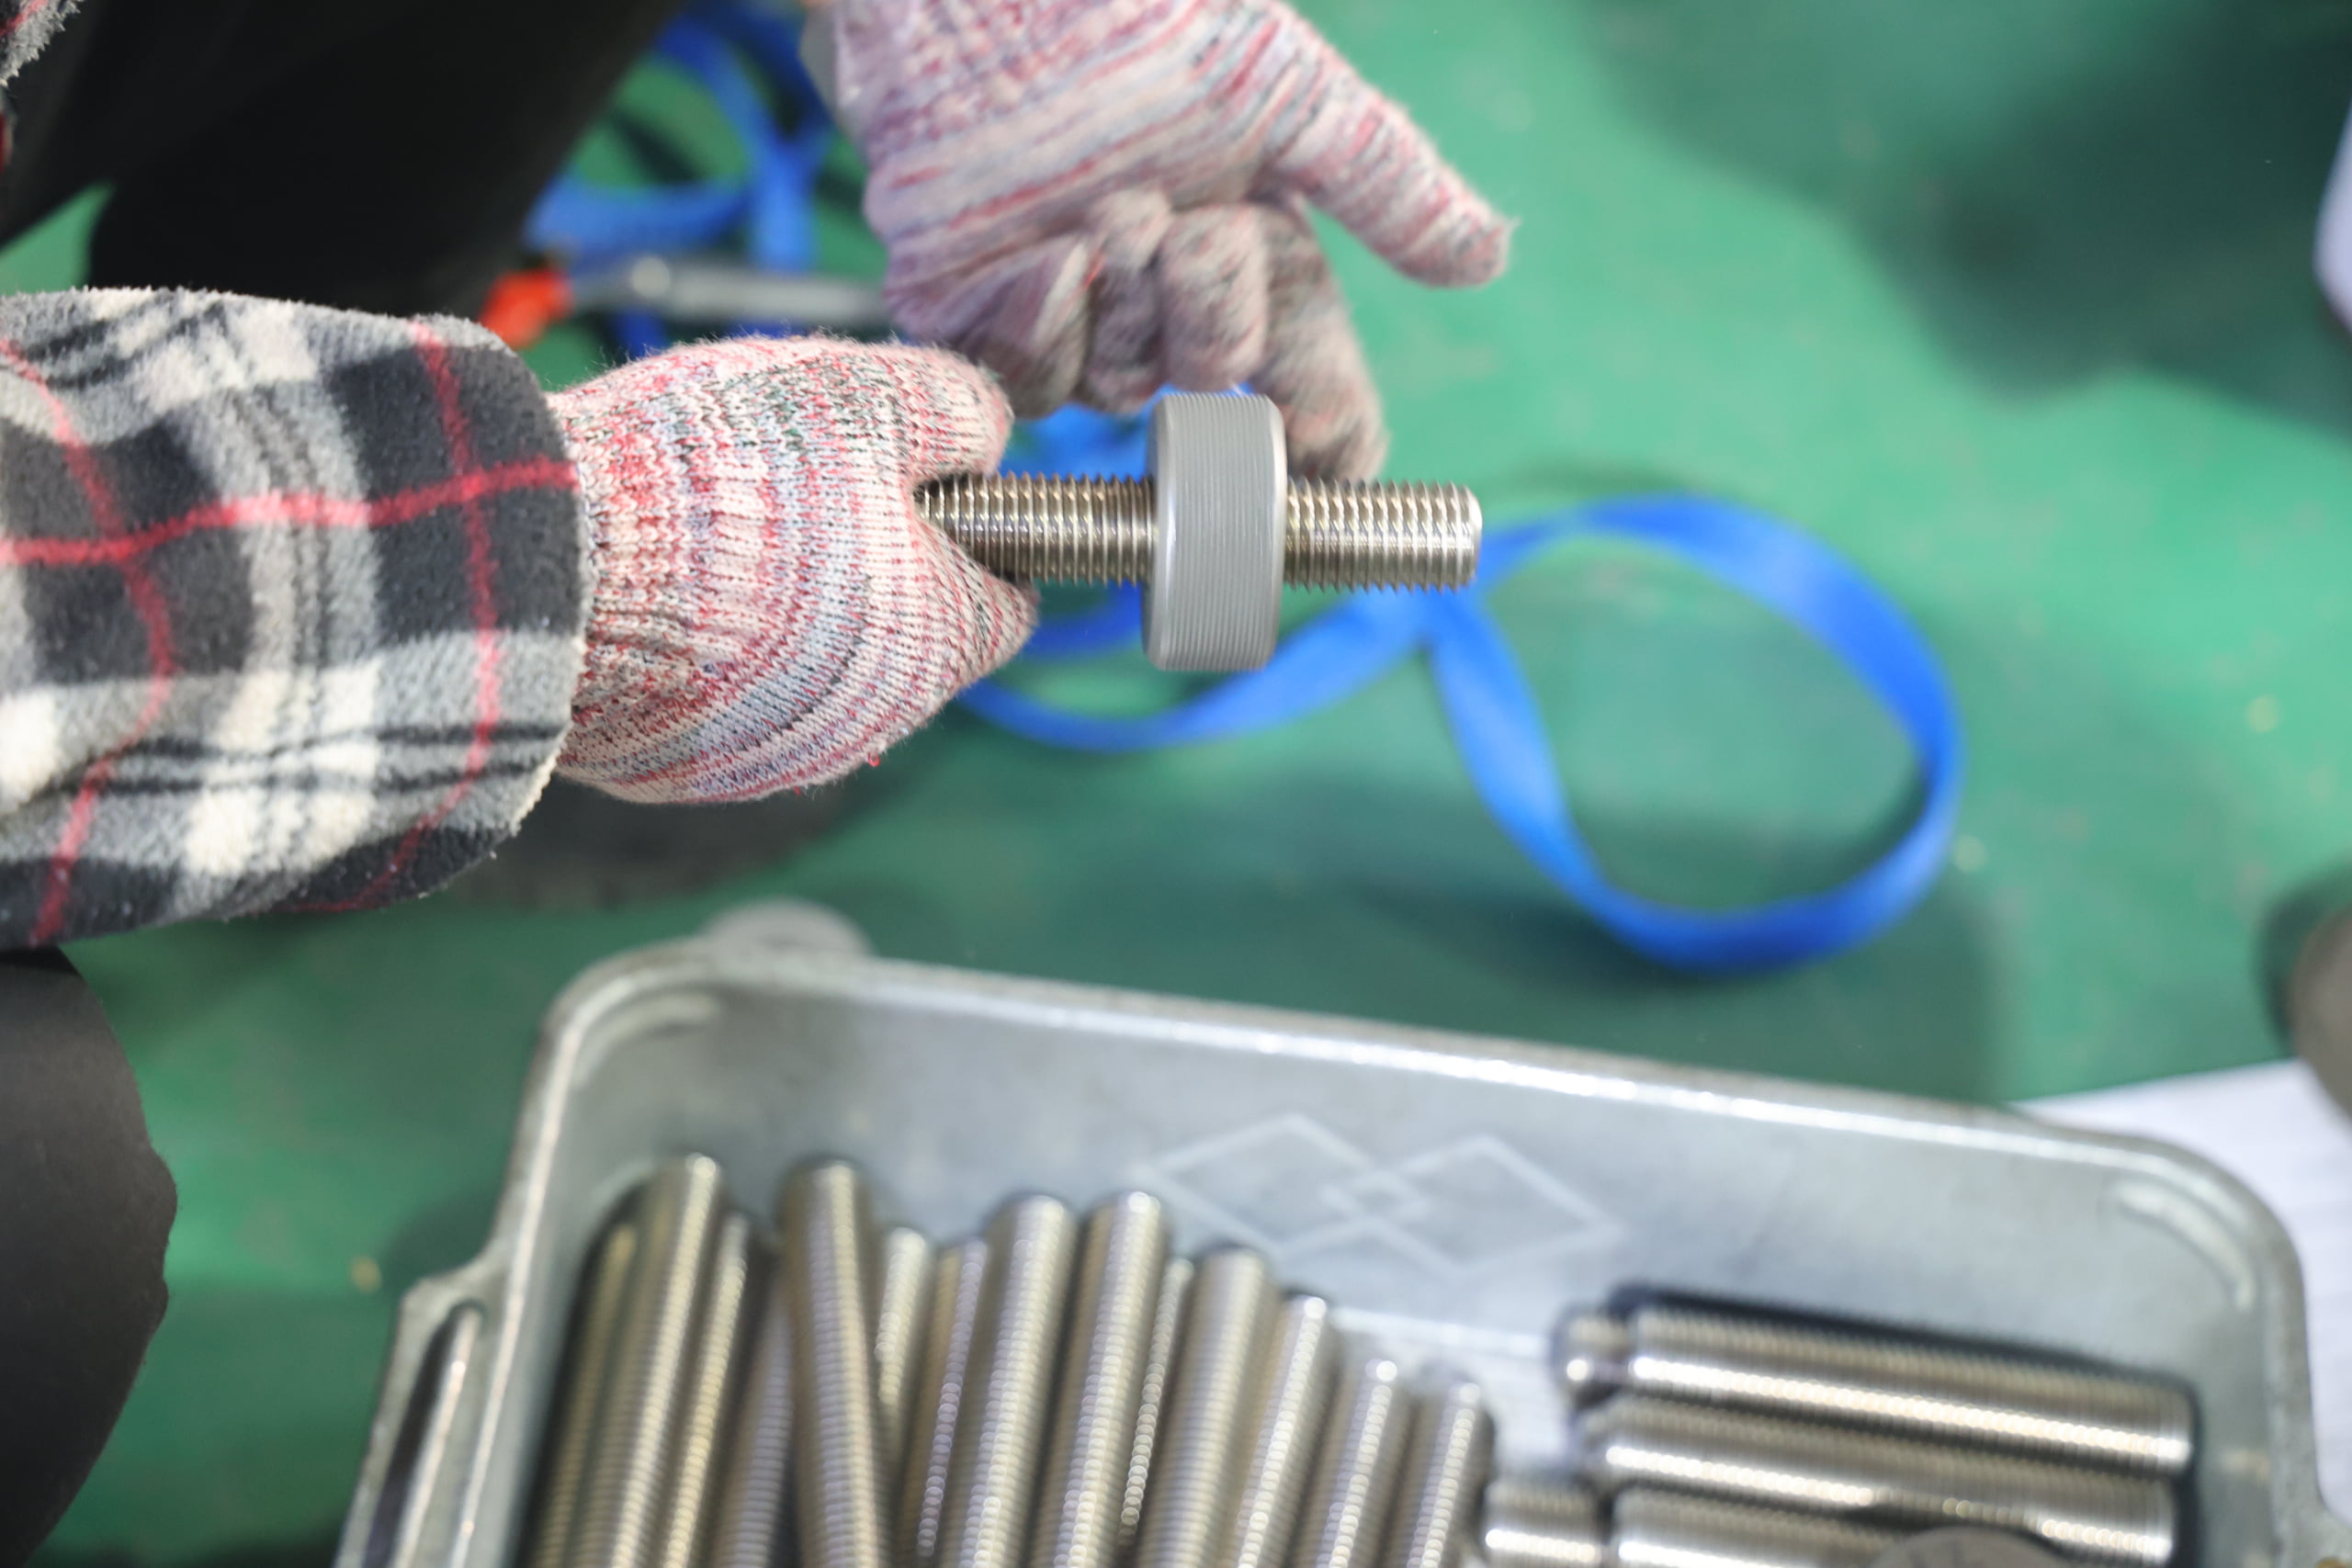
Critical dimensions, tolerances and product geometry are checked against the applicable dimensional standard or customer drawing.
Thread size, pitch and fit are verified using suitable gauges and measuring equipment. Additional profile verification can be arranged when specified.
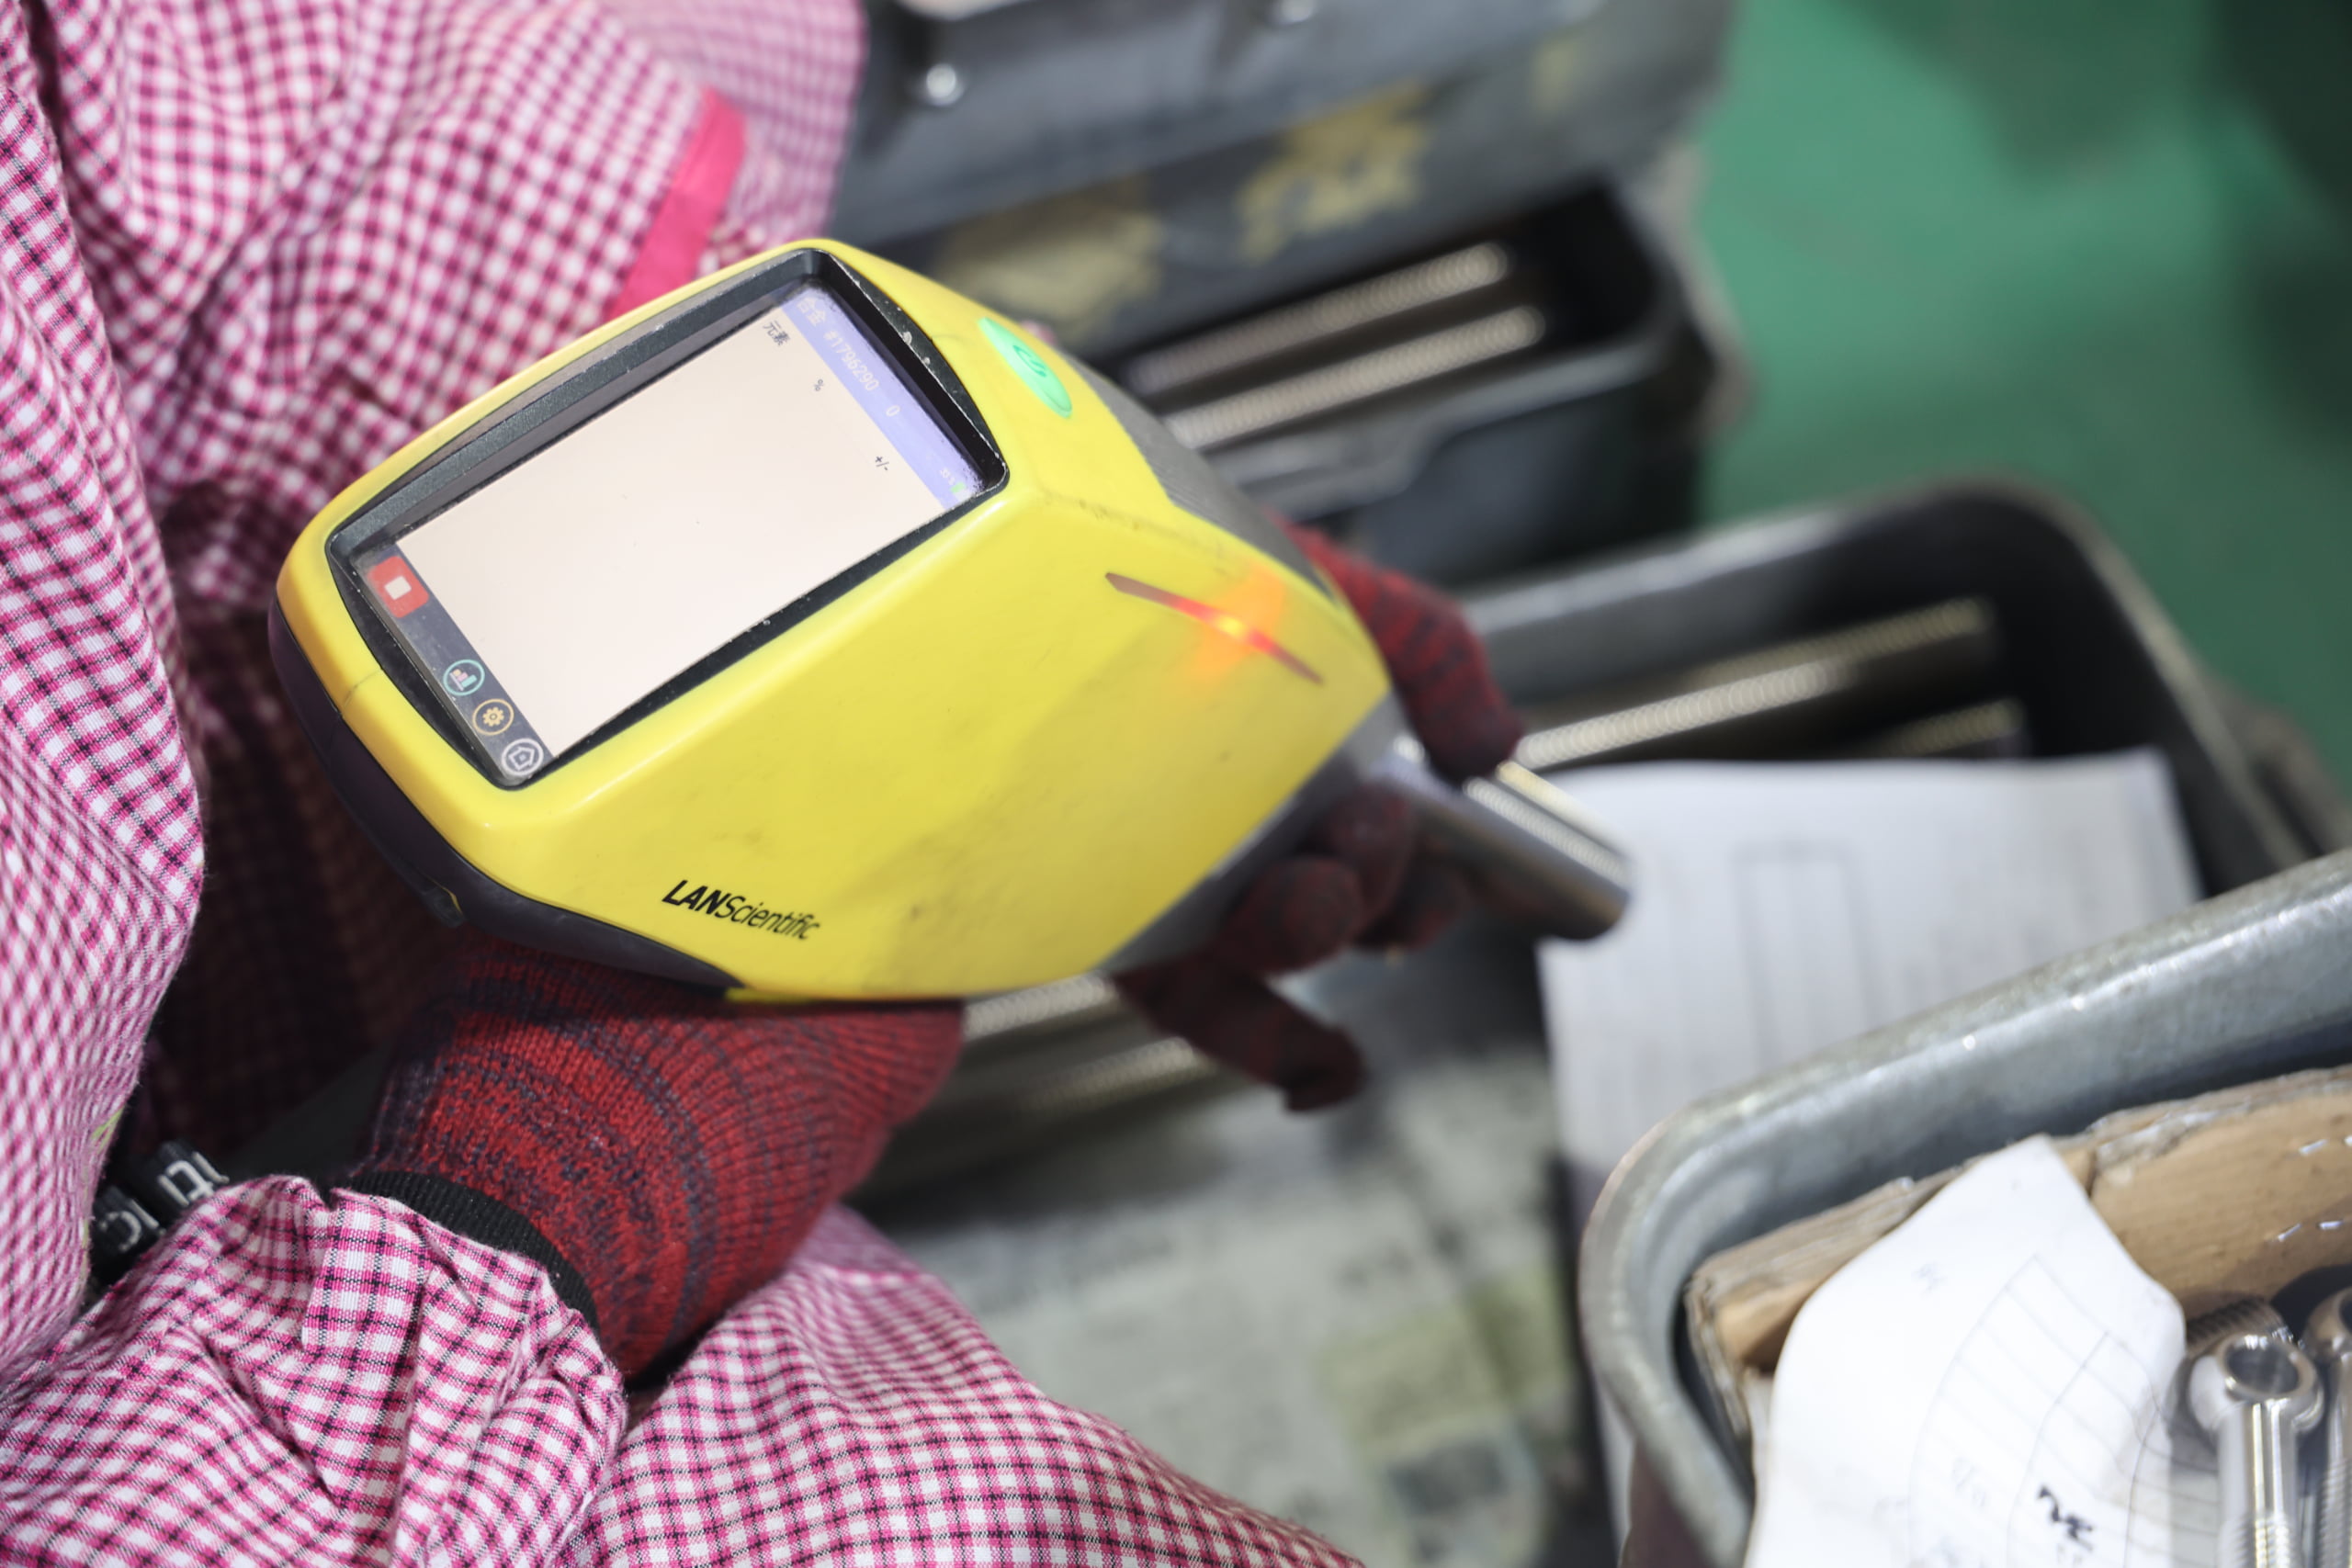
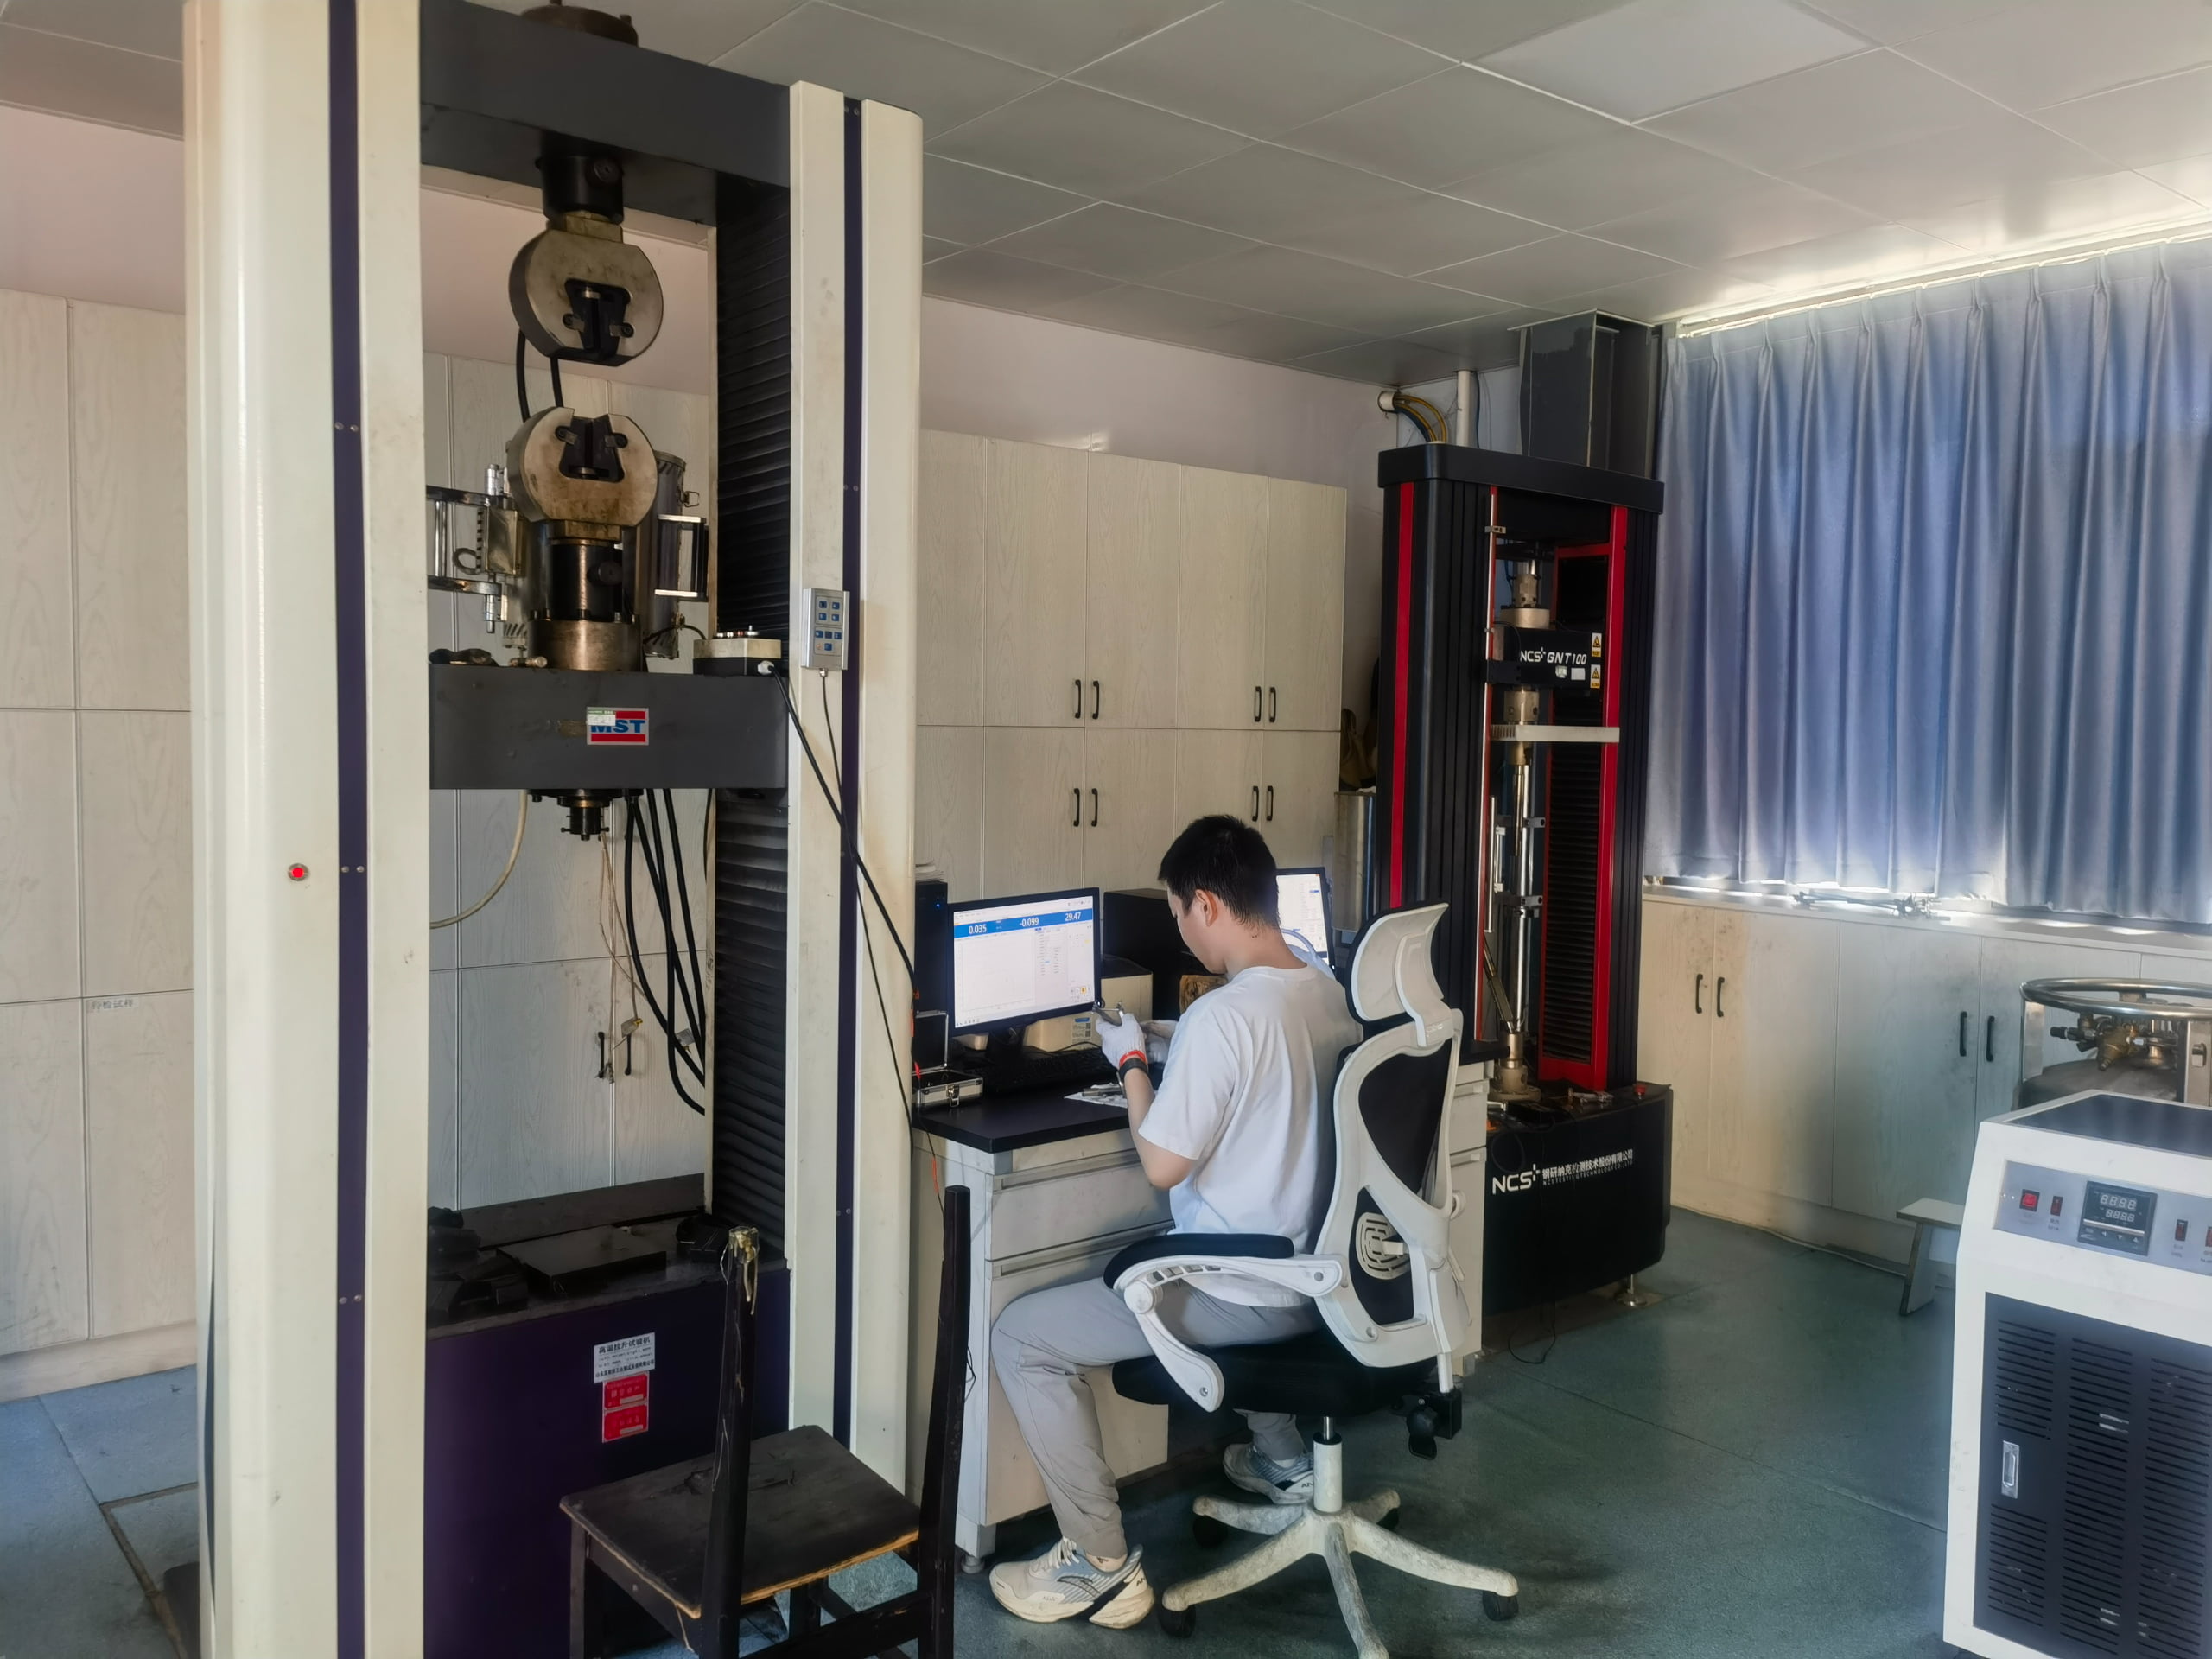
PMI, hardness, tensile or other testing can be performed or arranged when specified, depending on the material, test method and project requirements.
MTC / EN 10204 3.1 documentation, dimensional reports, PMI reports and traceability records can be supplied when specified and applicable.
Inspection methods, sampling plans, acceptance criteria and document requirements should be confirmed before order placement.
Discuss Inspection & Documentation RequirementsOur specialty-alloy fasteners support demanding projects across multiple industries. Final material selection must be based on the actual temperature, corrosion medium, mechanical load, applicable standards and required service life.
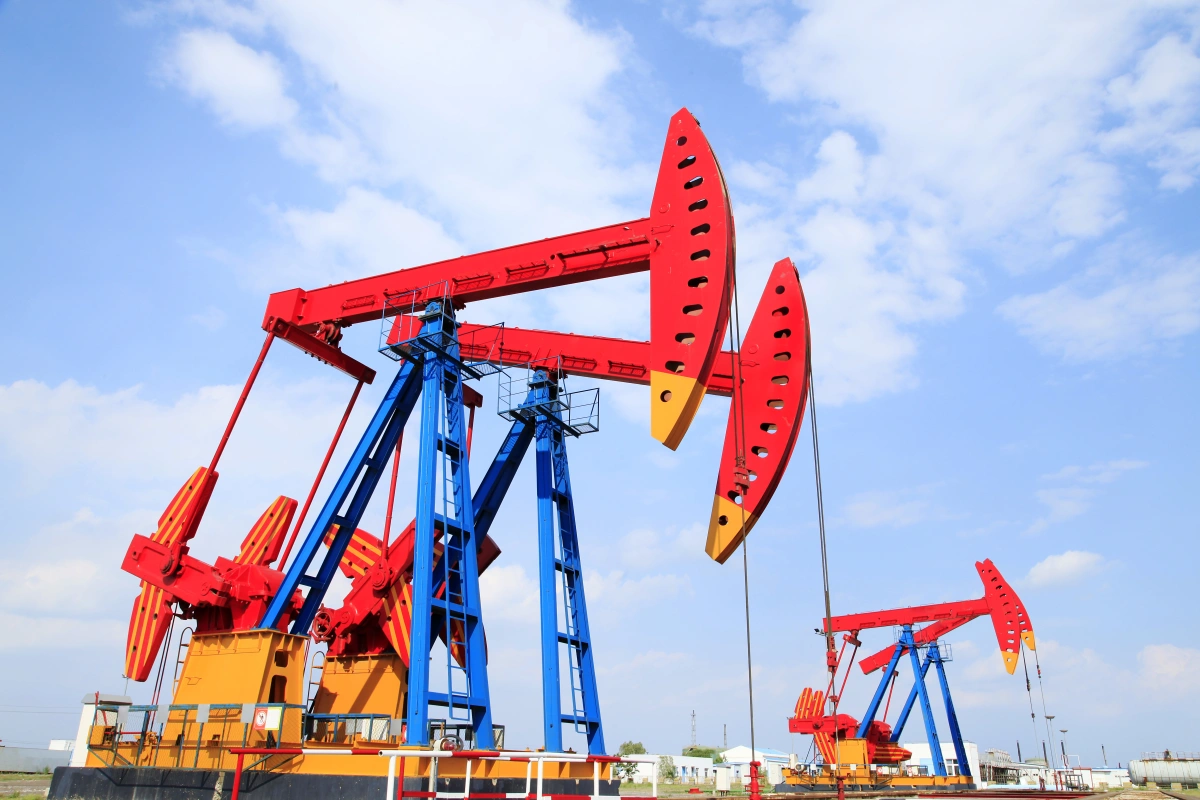
Flange bolting, valves, pressure equipment, piping systems and process units exposed to pressure, temperature or corrosive media.
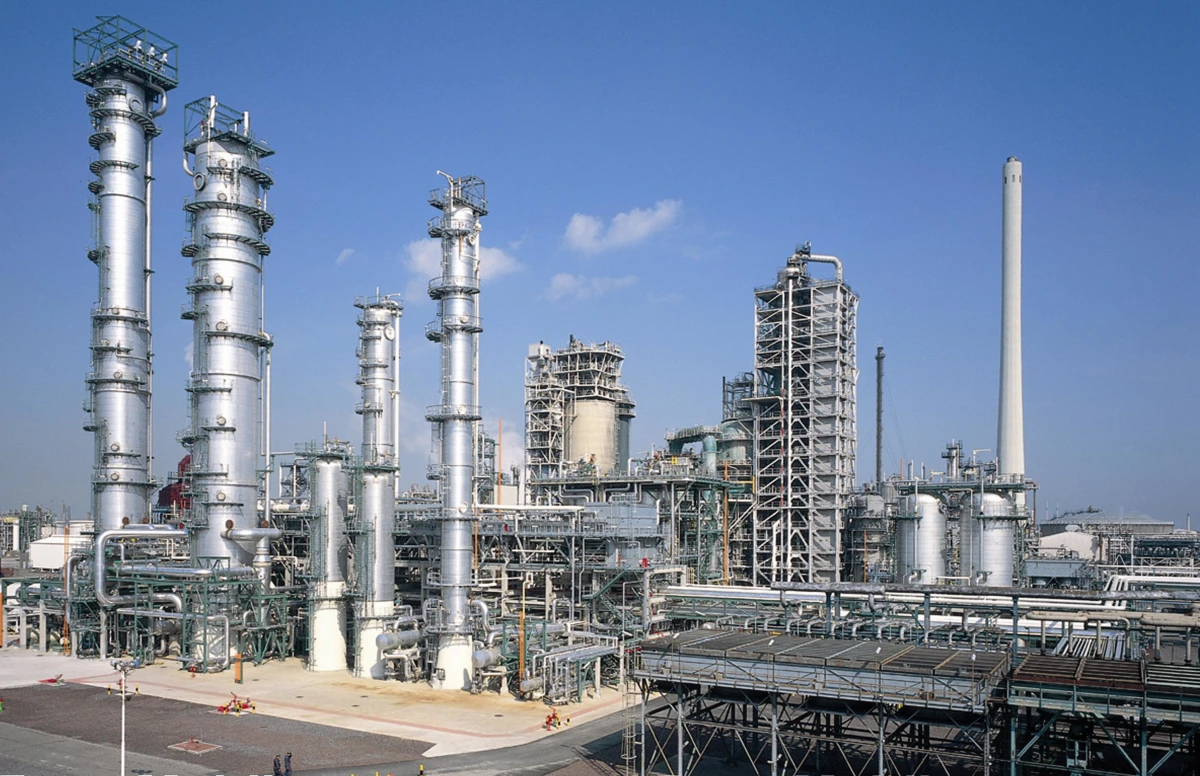
Reactors, heat exchangers, scrubbers, pumps and equipment handling acids, chlorides or other aggressive process media.
Gas and steam turbines, boilers, furnaces, heat-treatment systems and high-temperature mechanical assemblies.
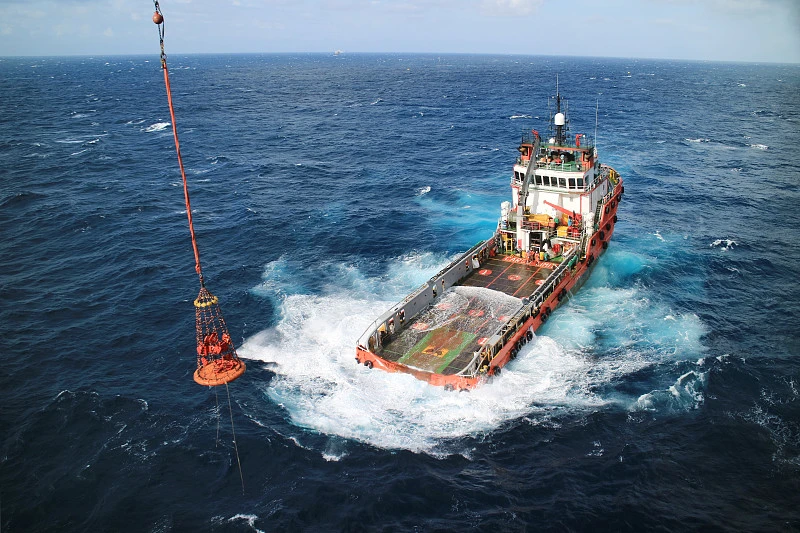
Offshore platforms, seawater systems, marine equipment and desalination installations requiring corrosion-resistant fastening.
Engine, thermal and precision assemblies requiring high strength, temperature capability, low weight or controlled material performance.
Safety-critical bolting and engineered components requiring controlled materials, documentation and reliable long-term performance.
Not every alloy is suitable for every industry or service condition. Material suitability should be confirmed against the governing specification and actual operating environment.
Discuss Your ApplicationCommon questions about specialty-alloy fasteners, custom manufacturing, standards, inspection, documentation and procurement.
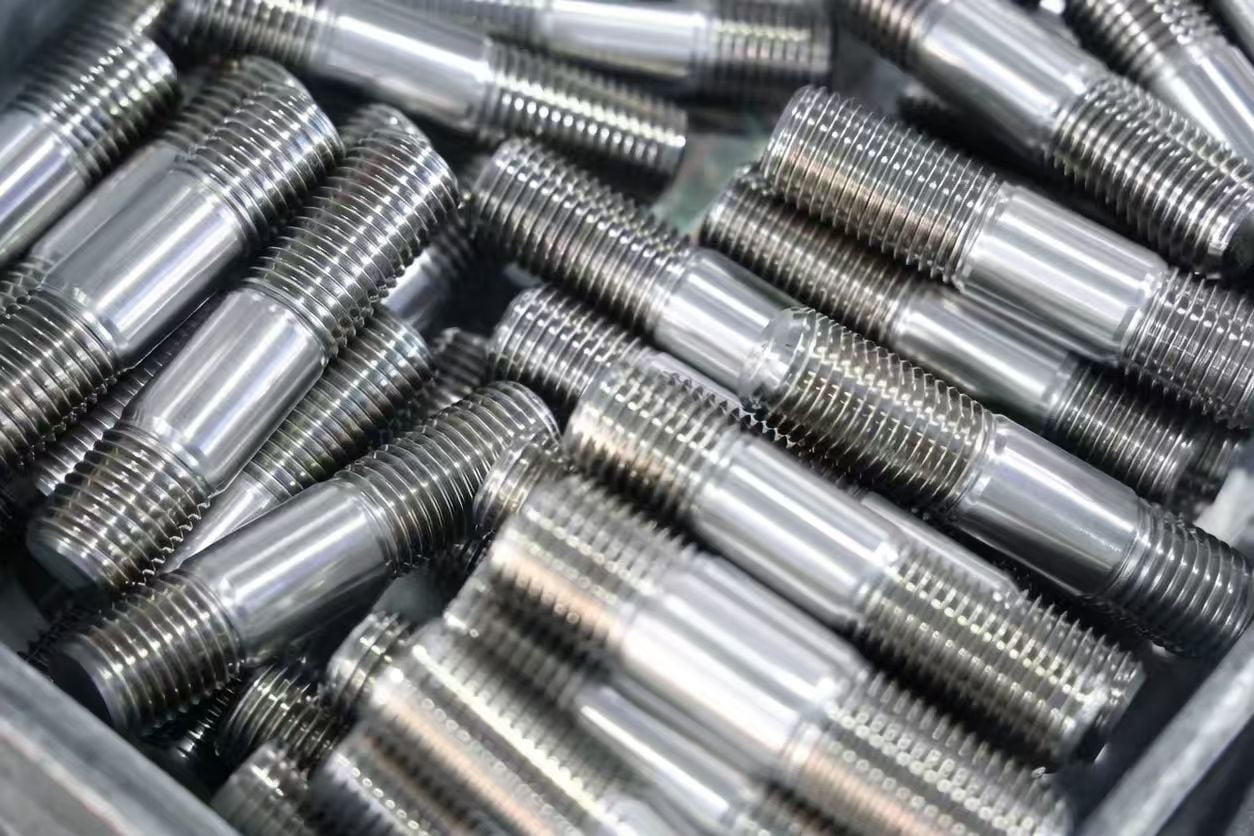
Send us your Specialty Austenitic Stainless Steel fastener specifications, standards or drawings. Our engineering team will review your requirements and provide a detailed project-specific quotation.
Fill out the form below or email us directly with your drawings.